Product Description:
Most people assume you machine a valve spool from solid bar stock, and plenty of shops still do it that way. We don’t. We cold head the blank first, which sounds like a small difference but actually changes the whole game. The grain structure of the steel flows around the contours rather than getting cut through, so you end up with a spool that handles cyclic pressure way better than a machined-only part. Once the basic shape is formed, we move to our CNC lathes and grinders to bring the critical diameters into spec, typically holding ±5 microns on the sealing lands. The surface finish we aim for sits around Ra 0.4, which gives you that nice smooth sliding feel without any stick-slip chatter. We also put a thin manganese phosphate coating on every spool, mainly to stop rust during shipping but it also helps with initial break-in.
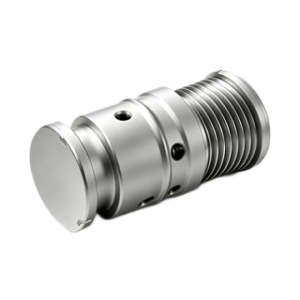
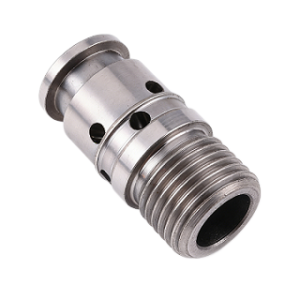
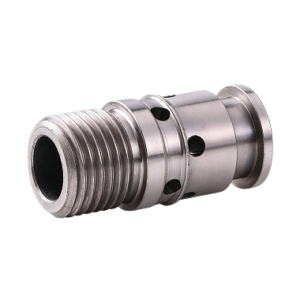
Specification:
| Product Name: | Item No.: | Material | Measurement(mm): | Surface Finish: | Weight(g): | ||
| L | W | Dia | |||||
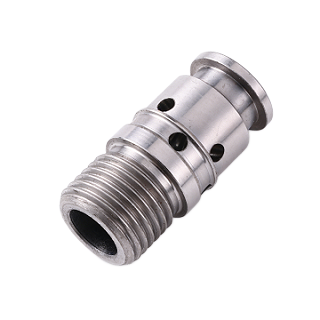
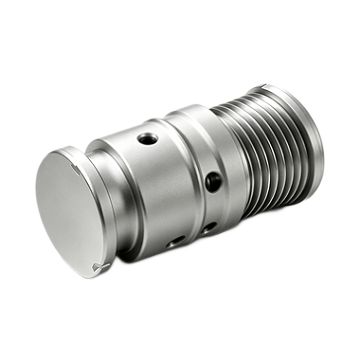
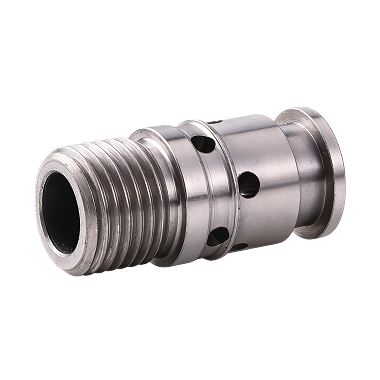
| Precision Hydraulic Valve Spool Cold Heading Formed Steel CNC Machined | QM1109 | Steel | 29 | / | Out D:13.45 Inner D1:7.76 Inner D2:25.8 |
Polish | 15.88 |
Products Details:
The Precision Hydraulic Valve Spool Cold Heading Formed Steel CNC Machined work well in real systems. Ours fall into the second category because we obsess over the little things that most shops ignore. The transition corners between the lands and grooves, for instance, we break those with a controlled radius instead of leaving them sharp. Sharp edges promote cavitation when oil velocity picks up, and cavitation eats away at the surface over time. Not good. Our metering notches, whenever the drawing calls for them, get finished on an EDM machine to ensure the pressure drop characteristics stay consistent from piece to piece. We also etch a serial number onto each spool before shipping, not because anyone asked, but because we archive inspection data for every single unit. If you call us five years from now asking about a specific batch, we can pull up the records in about two minutes. Try getting that from a trading house.
Product Feature:
-
The cold heading step isn’t just for show. It aligns the grain flow with the spool contour, which translates to roughly 30% better fatigue resistance compared to machining from round bar. We’ve tested this side by side, the numbers don’t lie.
-
Our grinding process leaves the lands and grooves consistent across the entire length. This matters because uneven metering edges lead to jerky cylinder movement, and nobody wants that.
-
Material-wise, we typically use 20CrMo or 16MnCr5, case-hardened to about 0.8-1.0mm depth. Core hardness sits around 30 HRC, surface hits 60 HRC after heat treat. Good balance of toughness and wear resistance.
Product Application:
-
Construction equipment. Excavators, loaders, telehandlers. The joystick controls need spools that meter smoothly, because operators notice any stickiness right away. We grind the lands carefully for these.
-
Industrial presses. Stamping and molding lines that run all day long. These spools cycle fast and hold up under pressure. One customer switched to us after burning through three sets from another shop in two years.
-
Marine. Steering systems and deck winches. Saltwater eats standard finishes, so we do an extra corrosion treatment on these. One extra step, doubles the service life.
-
Agriculture. Tractors and combines. Dust, heat, cold, vibration. These spools just keep working.
-
Test rigs. Flight simulators and materials testers. Low hysteresis is everything here.
Reviews
There are no reviews yet.