https://youtu.be/CTVkFCmQG-c?si=gyZUUL4IyQVTFW-F
Product Content:
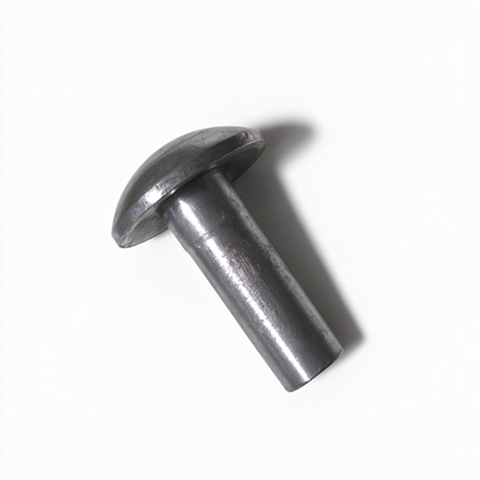
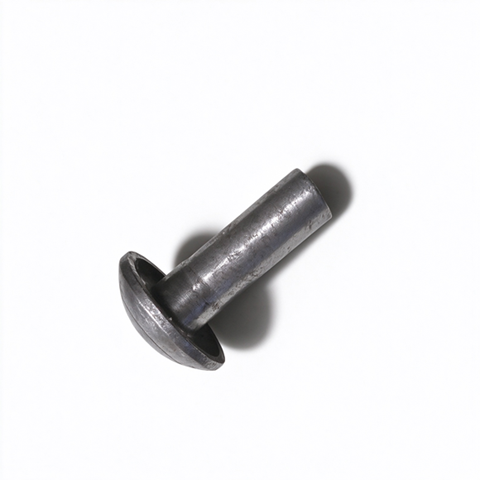
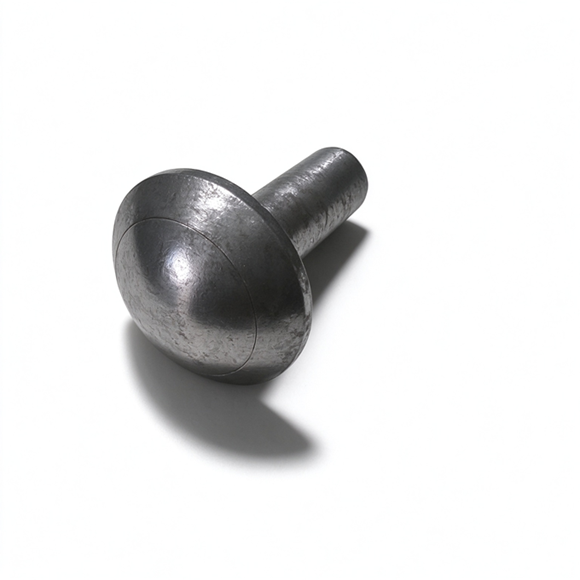
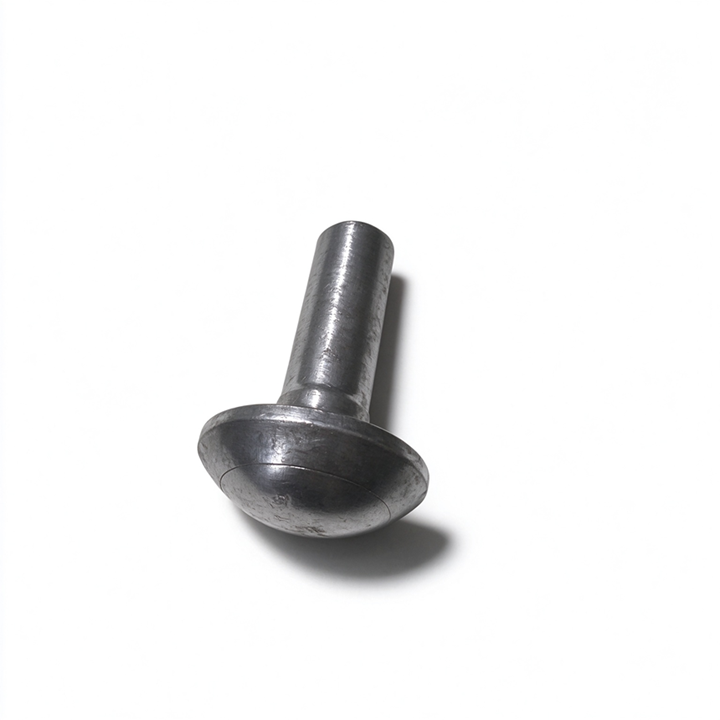
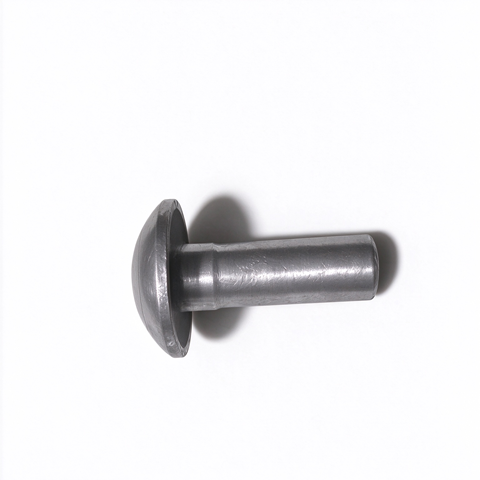
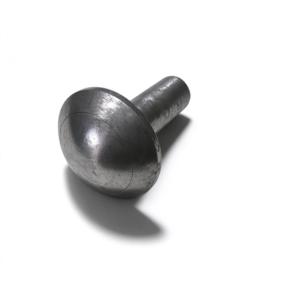
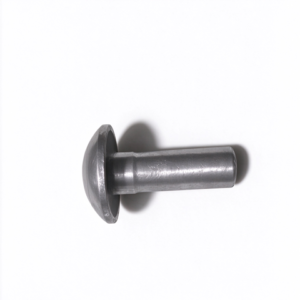
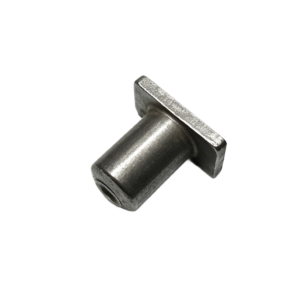
The Round Head Solid Rivet | DIN 660 Snap Head Rivet Manufacturer from Qimao Metal Manufacturer . The standard covers nominal diameters 1 mm through 8 mm, semi-circular head geometry, and shank tolerance class h11. The head is not decorative—its bearing area is calculated to distribute clamping force without dimpling thin sheet. Shank material options: steel (zinc plated or bright), stainless A2/A4, aluminum, copper. If you are joining dissimilar metals, the rivet material must be chosen against the base material to avoid galvanic couple. The solid cross-section is the whole point: tubular and blind rivets carry shear through a hollow wall, solid rivets carry it through the full diameter.
Product Specification:
| Product Name: | Item No.: | Material: | Measurement(mm): | Surface Finish: | Weight(g): | ||
| L: | W: | D: | |||||
|
Round Head Solid Rivet | DIN 660 Snap Head Rivet Manufacturer |
QM9031 | Steel | 47.82 | 31.62 | 12.73 | Blank | 71.51 |
Product Details:
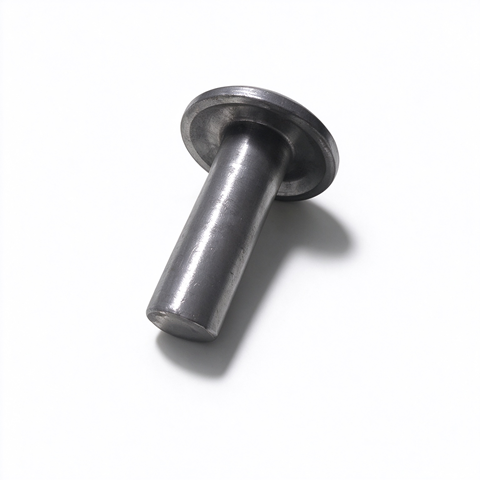
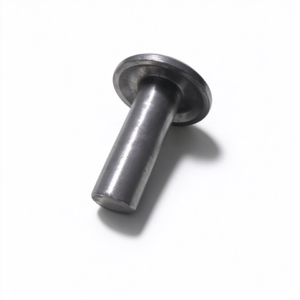
The product Round Head Solid Rivet | DIN 660 Snap Head Rivet Manufacturer shank end carries a slight chamfer. This is not cosmetic. Without it, the rivet hangs on the hole edge during insertion, and you end up driving it through with a hammer—which work-hardens the shank head and causes cracking later. The head-to-shank transition radius is where shear failures initiate in substandard rivets. Cold heading preserves grain flow through that radius; machining from bar stock cuts the grain and creates a stress riser. For stainless A2/A4, passivation after heading is mandatory to restore the chromium oxide layer disrupted by tool contact. If your supplier skips passivation, the rivets will show surface rust in humid storage within weeks.
Core Feature:
-
Round Head Solid Rivet | DIN 660 Snap Head Rivet Manufacturer with solid shank carries full-section shear load:The entire cross-section resists shear. This is why solid rivets hold up in structural joints that see sustained load.
-
Permanent, vibration-proof joint:Once set, there is no thread to strip and no locking element to fail. The rivet cannot back out under vibration, which is why heavy equipment still specifies it over threaded fasteners.
-
h11 shank tolerance for a snug fit:The rivet slips into a drilled hole without slop. Clearance slop is a common cause of work-loose joints; h11 tolerance removes that variable before installation even starts.
-
Domed head spreads clamping force:The semi-circular bearing surface distributes force evenly across the joint, reducing the risk of dimpling thin sheet and leaving a finished appearance on exposed surfaces.
-
Cold-headed grain flow through the transition radius:Grain follows the head-to-shank contour instead of being cut across it. That radius is where substandard rivets initiate shear cracks under cyclic load.
-
Passivated stainless options:A2/A4 rivets are passivated after heading to restore the chromium oxide layer disrupted by tool contact, so they resist corrosion in humid storage and wash-down service.
Wide Usage:
-
Truck frame crossmembers and crane subassemblies:These joints of Round Head Solid Rivet | DIN 660 Snap Head Rivet Manufacturer carry shear under continuous vibration. A blind rivet may be faster to install, but it cannot match the solid shank’s load path—do not substitute just for speed.
-
Scaffold nodes and heavy equipment:Permanent structural connections where threaded fasteners may loosen over load cycles. Once set, the rivet stays tight for the service life of the assembly.
-
Tamper-evident panels and security enclosures:For closed installation, opening need drilling. Use on access panels and equipment cabinets, prevent unauthorized opening.
-
Architectural and visible hardware:The domed head sits proud with a finished look, appropriate for exposed surfaces. Specify stainless A4 for exterior or wash-down environments where corrosion resistance matters.
-
Aircraft and aerospace skin panels:A classic high-shear application where joint integrity is non-negotiable and every fastener is specified, not guessed.
-
Not for serviceable joints:If the assembly must be disassembled for maintenance, specify a threaded fastener or a removable blind rivet. Solid rivets are permanent by design, not by accident.
Setting Procedure:
Clamp the workpieces Round Head Solid Rivet | DIN 660 Snap Head Rivet Manufacturer. Any gap between sheets will show up as a loose joint after setting—the rivet cannot pull the sheets together; it only fills the hole. Drill the hole to nominal shank diameter, deburr both sides. Insert the rivet. Place the bucking bar flat and square against the protruding shank. The rivet set goes on the manufactured head; the gun must be perpendicular to the surface. Trigger in short bursts. The bucking bar resists the hammering; the shank expands and forms the shop head. Stop when the shop head diameter reaches about 1.5×d and height about 0.5×d. Inspect: no sheet separation, no cracked head, shop head centered on the shank axis. A tilted shop head means the gun was off-angle—drill it out and redo. Do not try to “tighten” a rivet by hitting it again after it has cooled.
Reviews
There are no reviews yet.