1. What Is Precision Cold Heading (and Why It Matters)
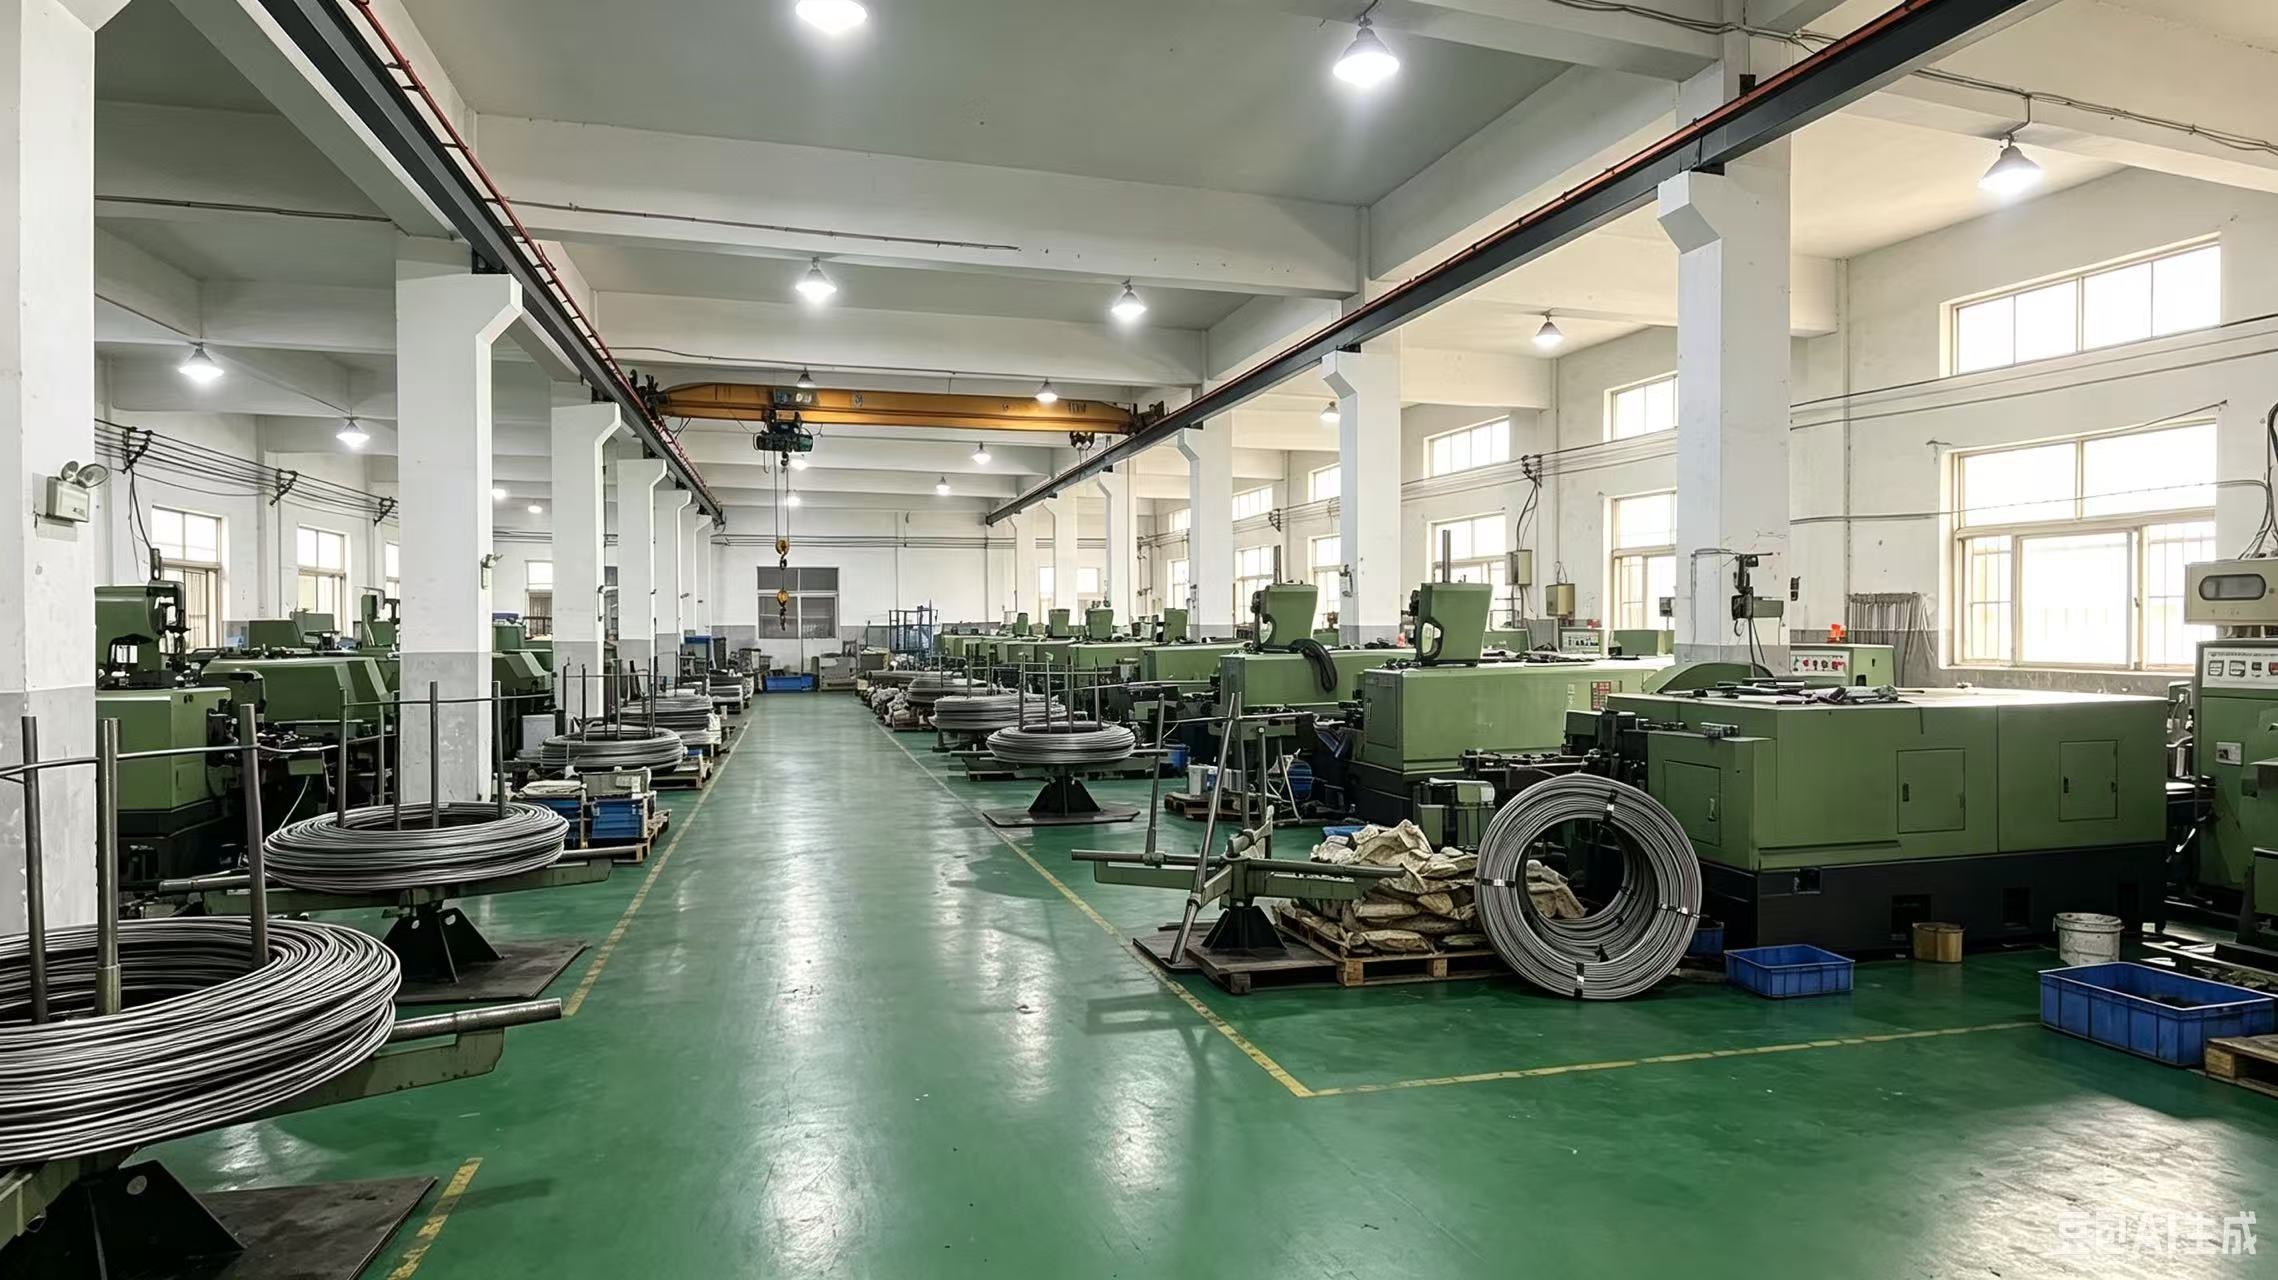
Cold heading (also called cold forming) is not a casting or stamping shortcut. It is a solid-state metal-forming process: a slug of wire or rod is cut to length, then forced through a series of progressive dies at room temperature. Each die station upsets, extrudes, pierces or trims the material one step at a time, transforming a simple cylinder into a finished — or near-finished — shape.
What makes this fundamentally different from machining is that no material is cut away. The metal is moved, not removed.
- Material utilization of 90–95% or more. A turned part can waste 40–70% of the raw bar as chips.
- Uninterrupted grain flow. The metal flows along the part’s contour, so cold-headed parts typically show higher fatigue strength and impact toughness than identical geometries machined from bar.
- Work hardening. Deforming the metal at room temperature raises its tensile and yield strength.
- High-volume repeatability. Progressive dies produce the same shape millions of times with tight control.
2. The New Technology: Cold Heading + CNC Finishing
For years, cold heading and CNC machining were treated as competitors. The modern approach — the one we’ve built our production around — treats them as two stages of one process:
- Stage 1 — Cold heading (near-net-shape): a multi-station machine forms the close-to-final geometry — heads, steps, flanges, undercuts, chamfers.
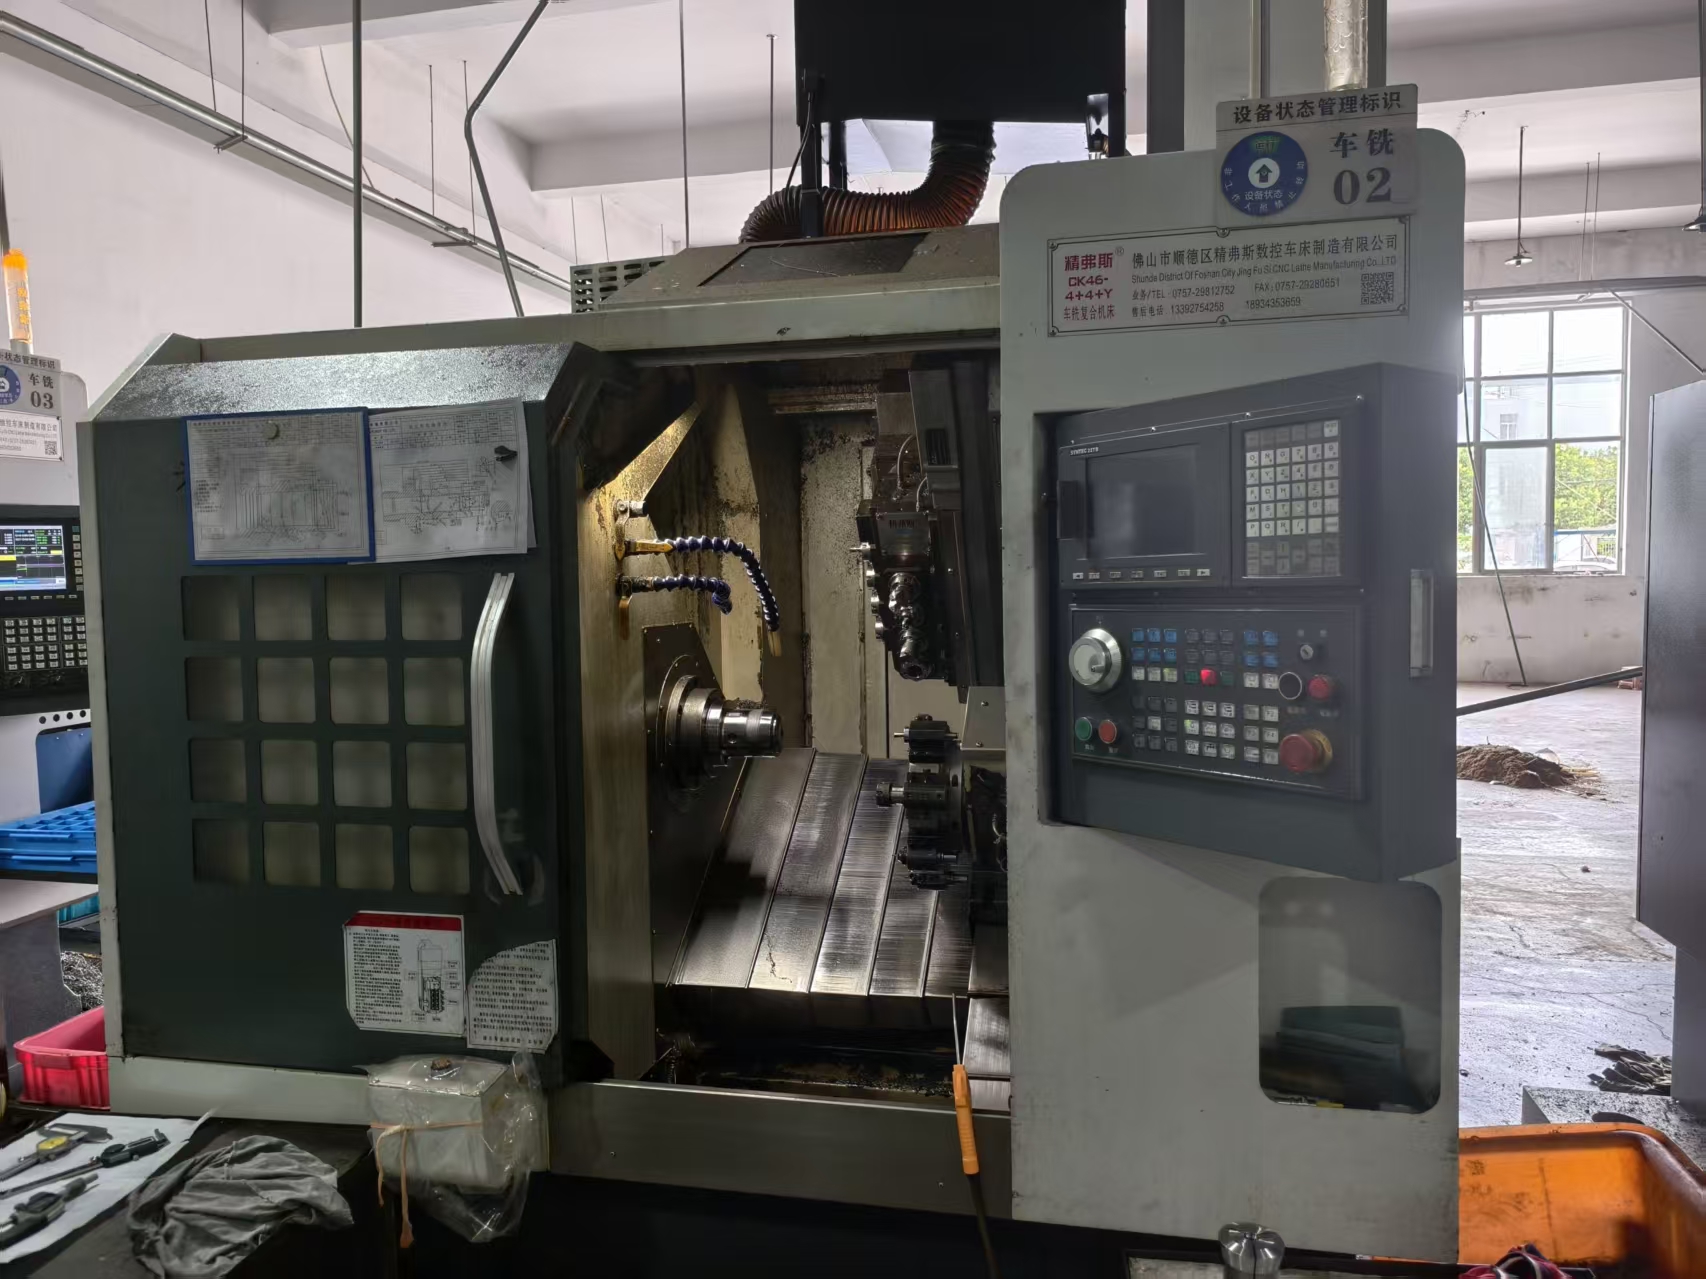
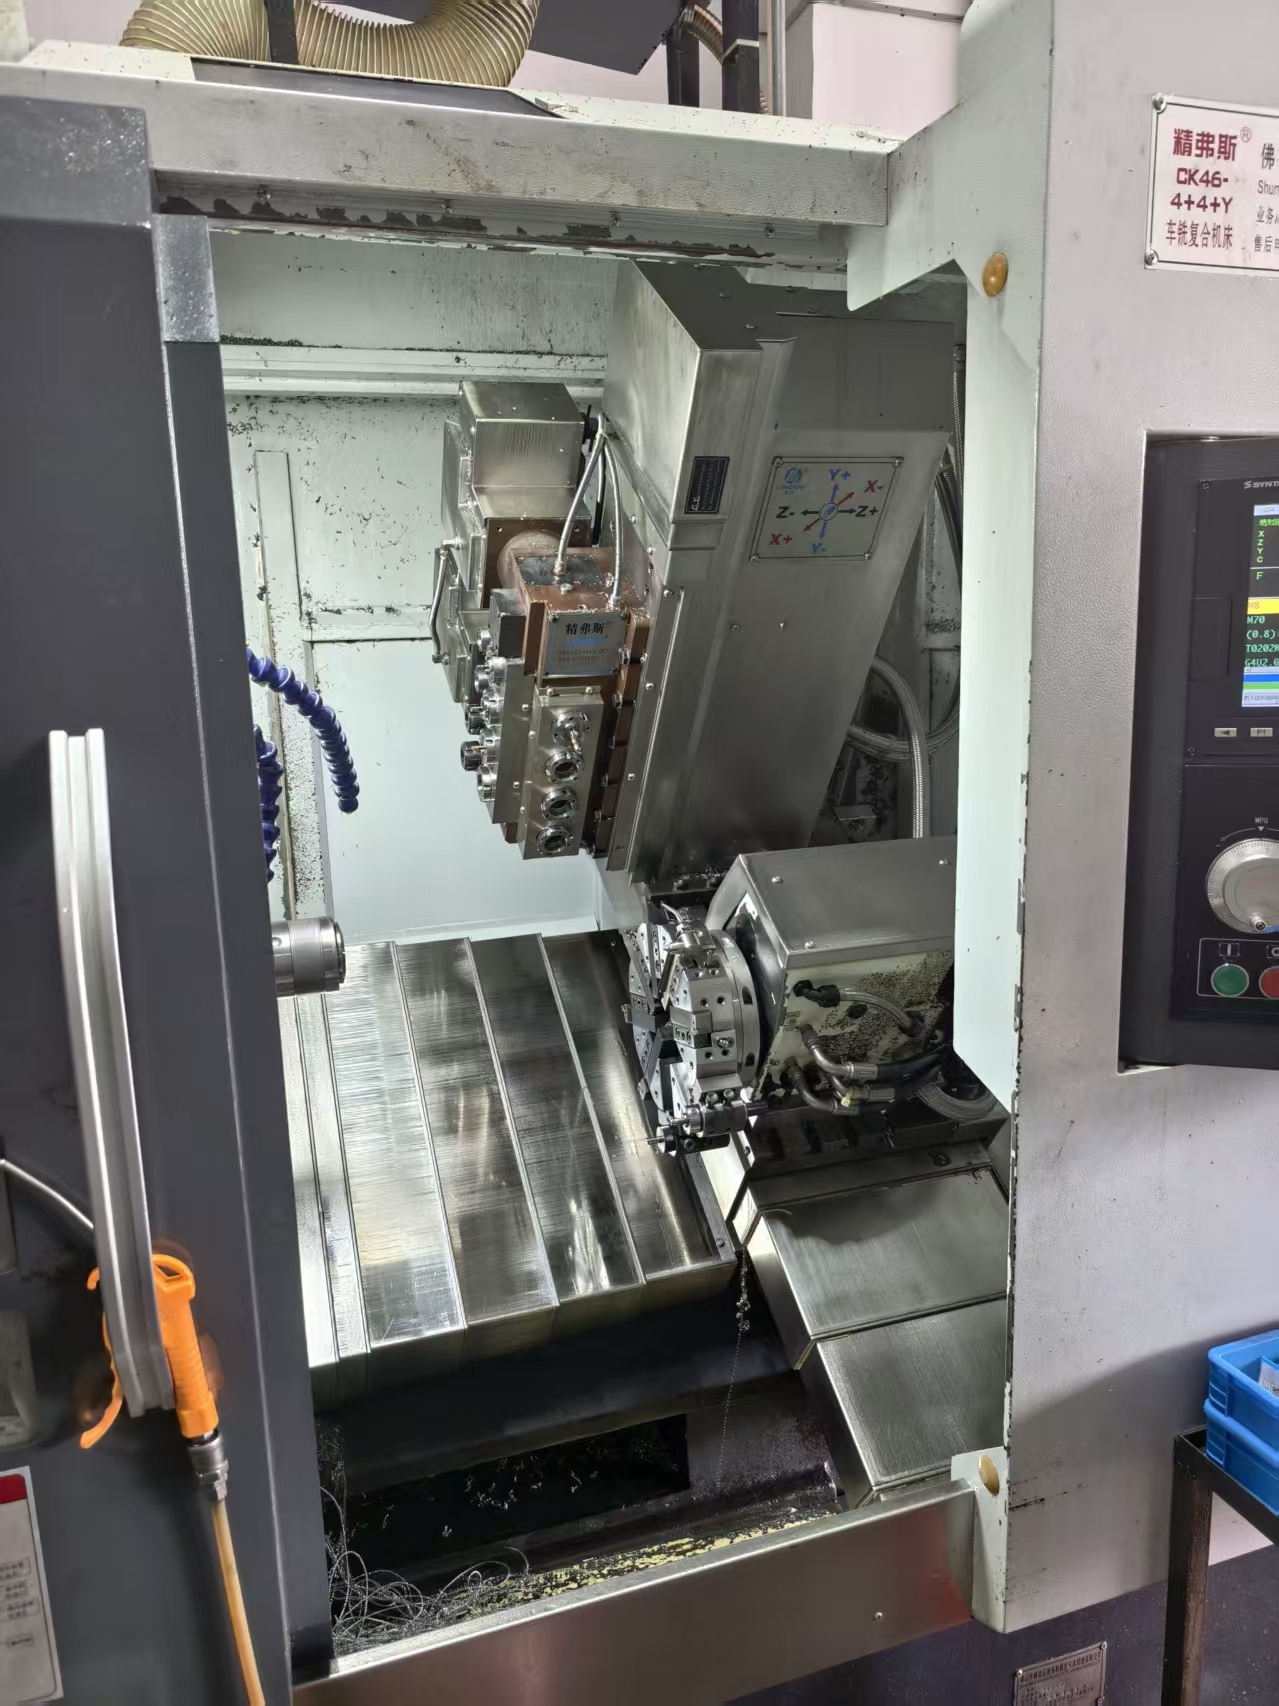
- Stage 2 — CNC finishing (precision): Swiss-type and 2-axis lathes, and 3-axis machining centers bring the part to final size with tight tolerances, fine finishes, threads, cross-holes and radii.
Why combine them? You get the strength and material savings of cold forming plus the precision of CNC turning — in one part that is cheaper, stronger and more consistent than either alone.
3. Cold-Headed vs. Fully Machined: A Practical Comparison
| Factor | Fully Machined | Cold Heading Only | Cold Heading + CNC |
|---|---|---|---|
| Material waste | High (40–70%) | Very low | Low |
| Grain flow / fatigue | Cut across grain | Excellent | Excellent |
| Tolerances | Good | Moderate | Tight (m6/h6 or better) |
| Surface finish | Good | Fair | Excellent (ground) |
| Cost at volume | High | Lowest | Low |
4. The Components This Technology Produces
4.1 Dowel Pins & Positioning Pins
Hardened ground dowel pins (DIN 6325 / ISO 8734 / ASME B18.8.2), cold-headed stepped/tabbed pins, hollow pins — for locating, alignment and shear load transfer.
4.2 Shaft Pins — Clevis & Hinge Pins
Clevis pins with cotter holes, hinge pins, custom stepped/headed pins for moving linkages and pivots.
4.3 Bushings — Bronze, Flanged, Split & Straight
Solid or oil-impregnated bronze, flanged, split and straight sleeves — bearings that take the friction so the shaft doesn’t have to.
→ Bronze · Flanged · Split · Straight
4.4 Fasteners — Bolts, Screws, Studs, Rivets & Nuts
Cold-formed, thread-rolled fasteners — the classic cold-heading application, done to engineered standard.
→ Bolts · Screws · Studs · Rivets · Nuts
5. Materials, Tolerances & Surface Treatments
| Category | Common Grades |
|---|---|
| Carbon steel | SWRCH series, 1018, 1045 |
| Alloy steel | SCM435, SCM440, 40Cr |
| Stainless steel | 304, 316, 420 |
| Aluminum & brass | 6061, 7075; brass |
| Bronze (bushings) | SAE 660 (C93200), sintered bronze |
Typical tolerances: linear ±0.01 mm; diameters to m6/h6 on ground pins; Ra 0.4–0.8 μm on ground surfaces. Heat treatment: quench & temper, carburizing, induction hardening. Finishes: zinc, nickel, black oxide, phosphating, passivation (RoHS options).
6. How Every Batch Is Verified
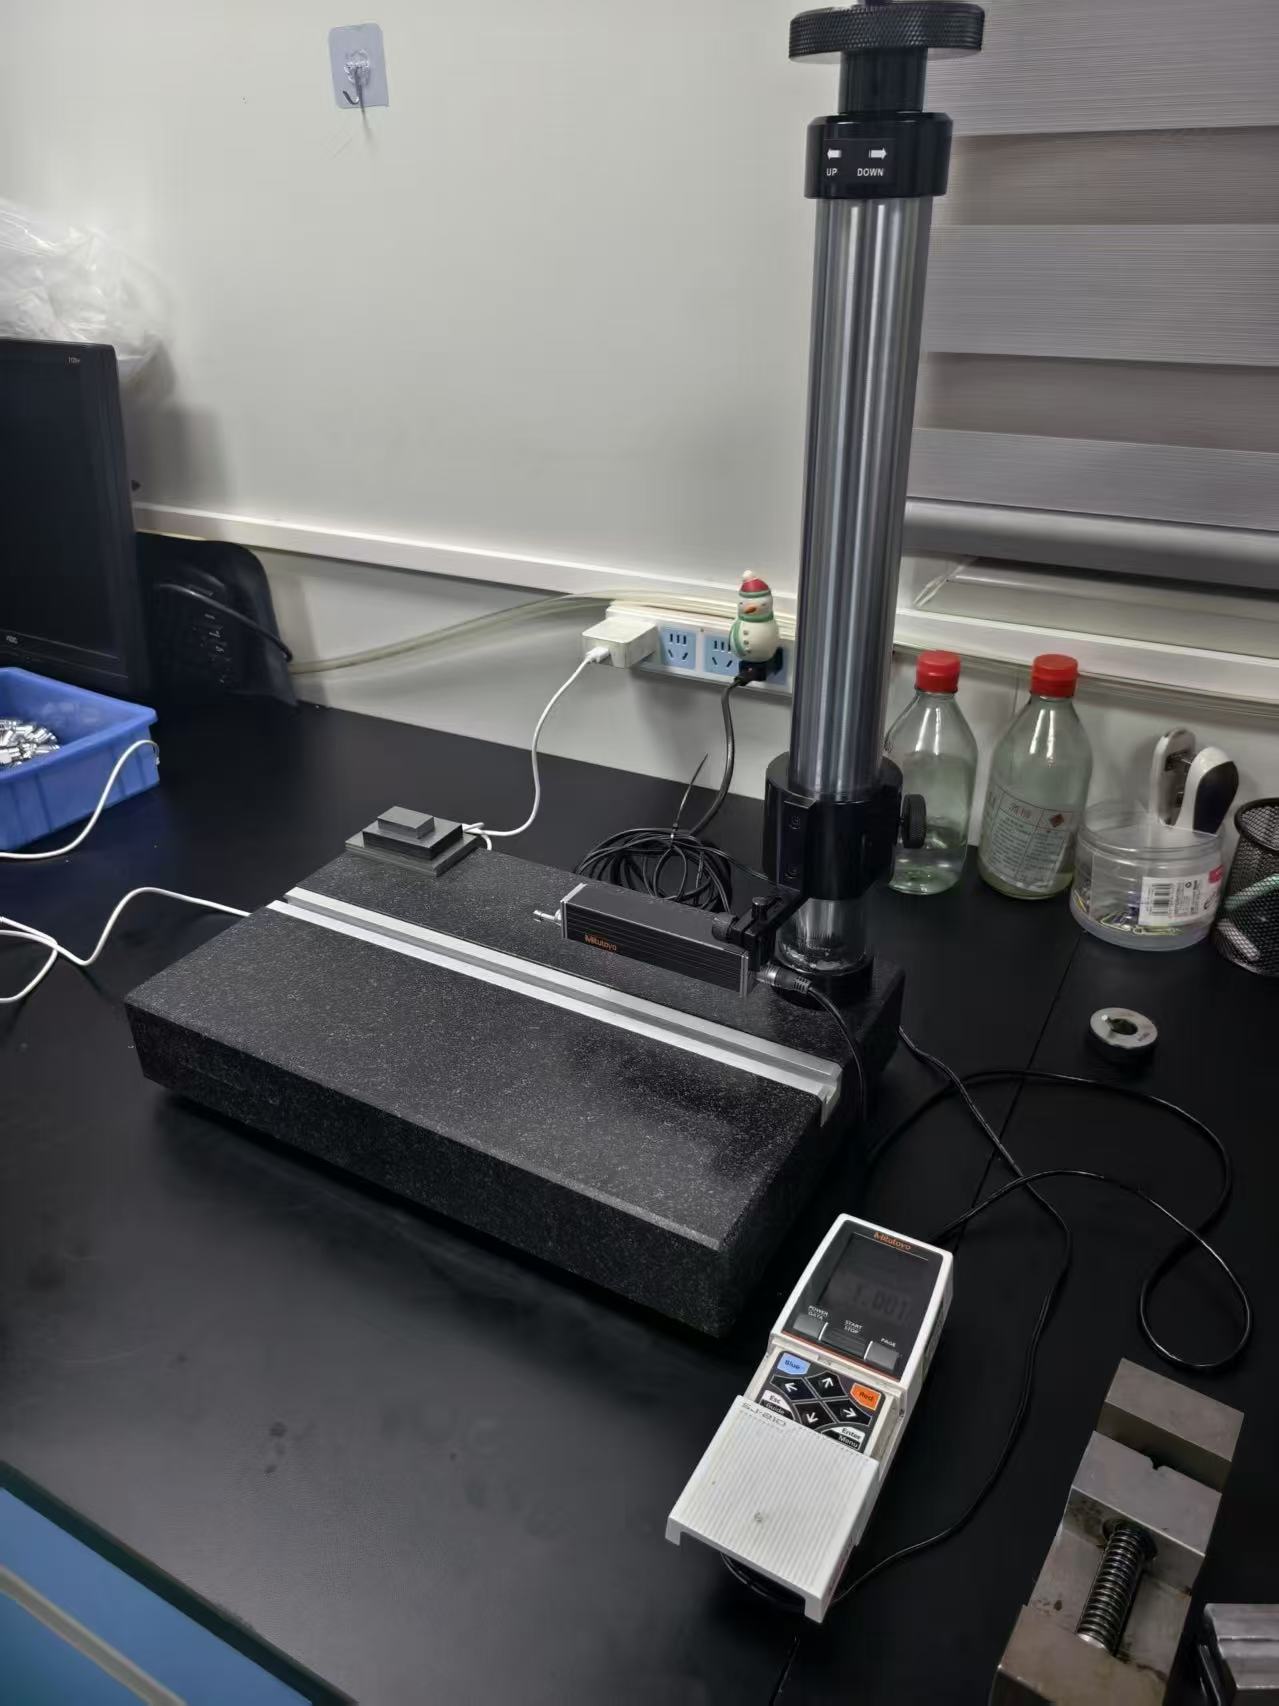
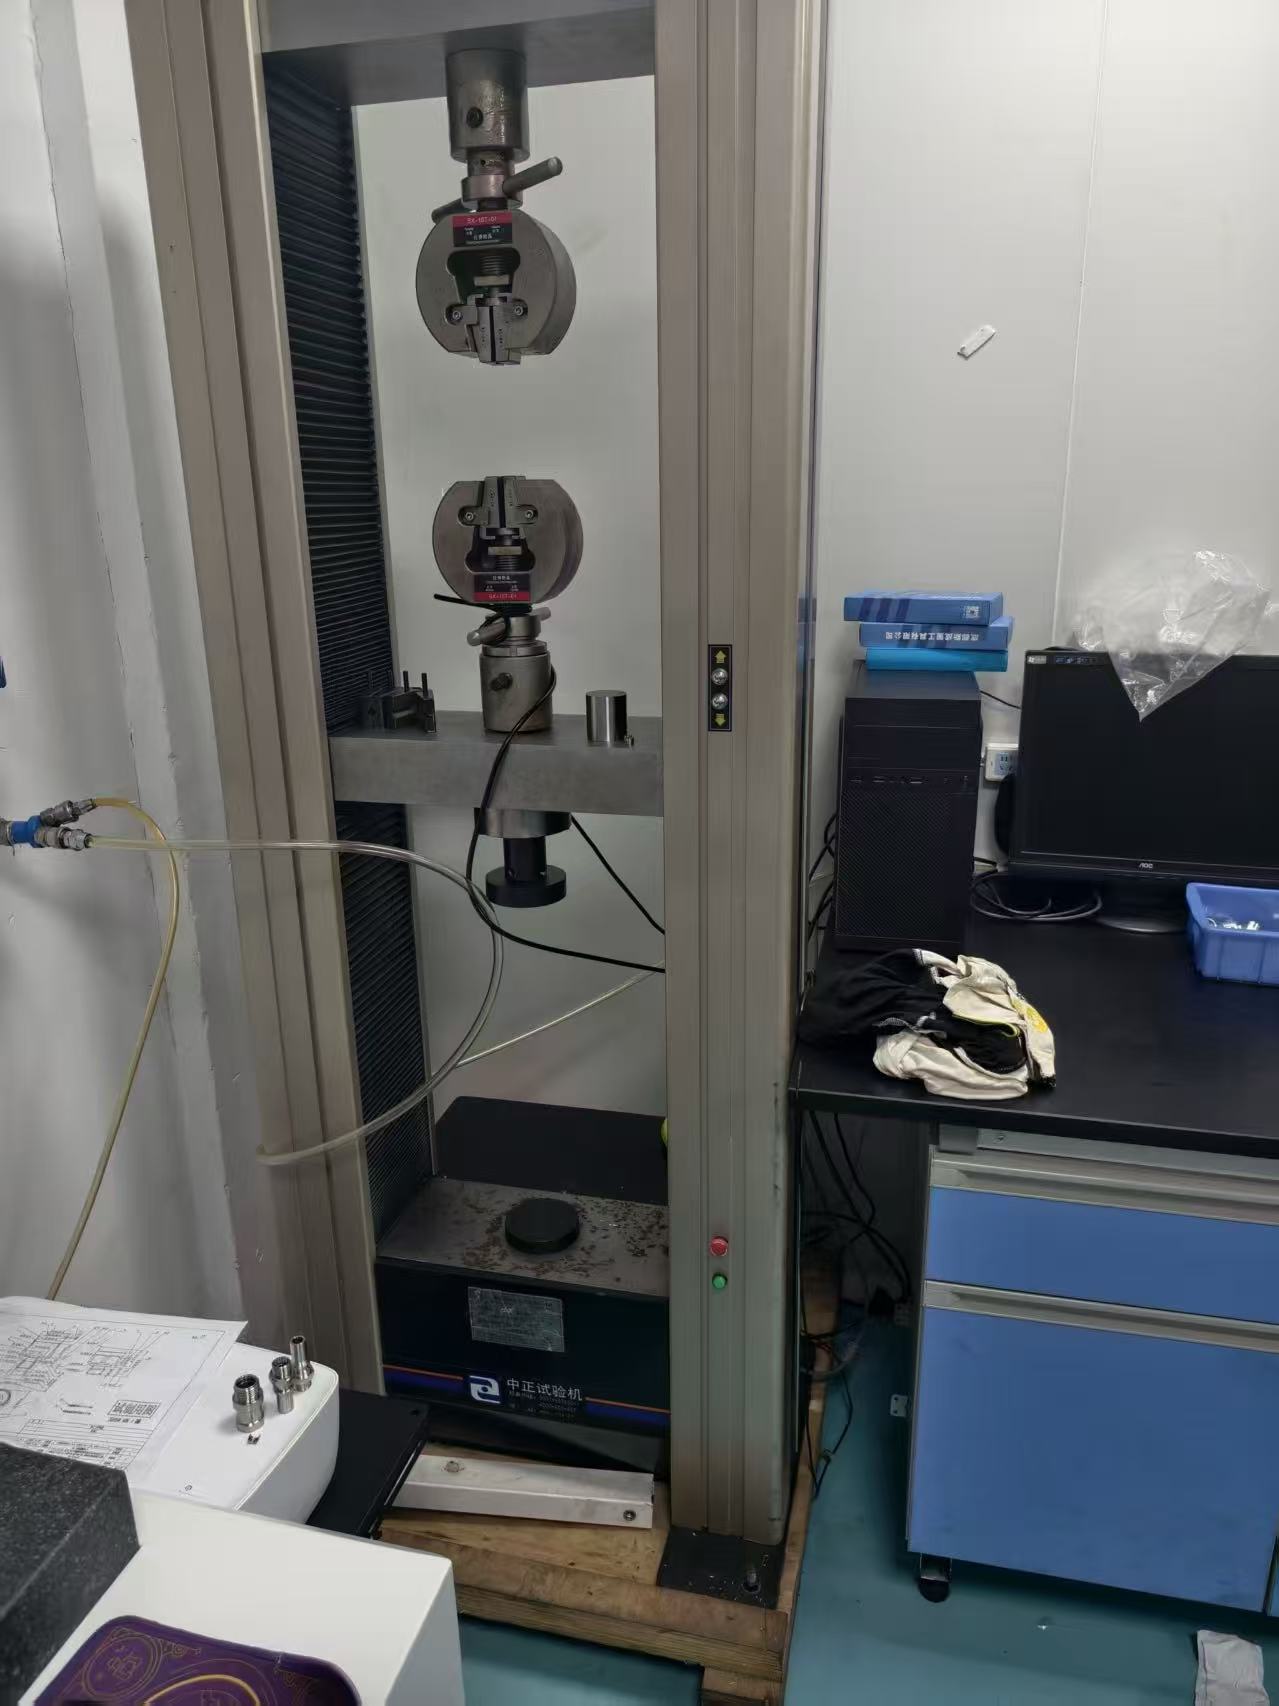
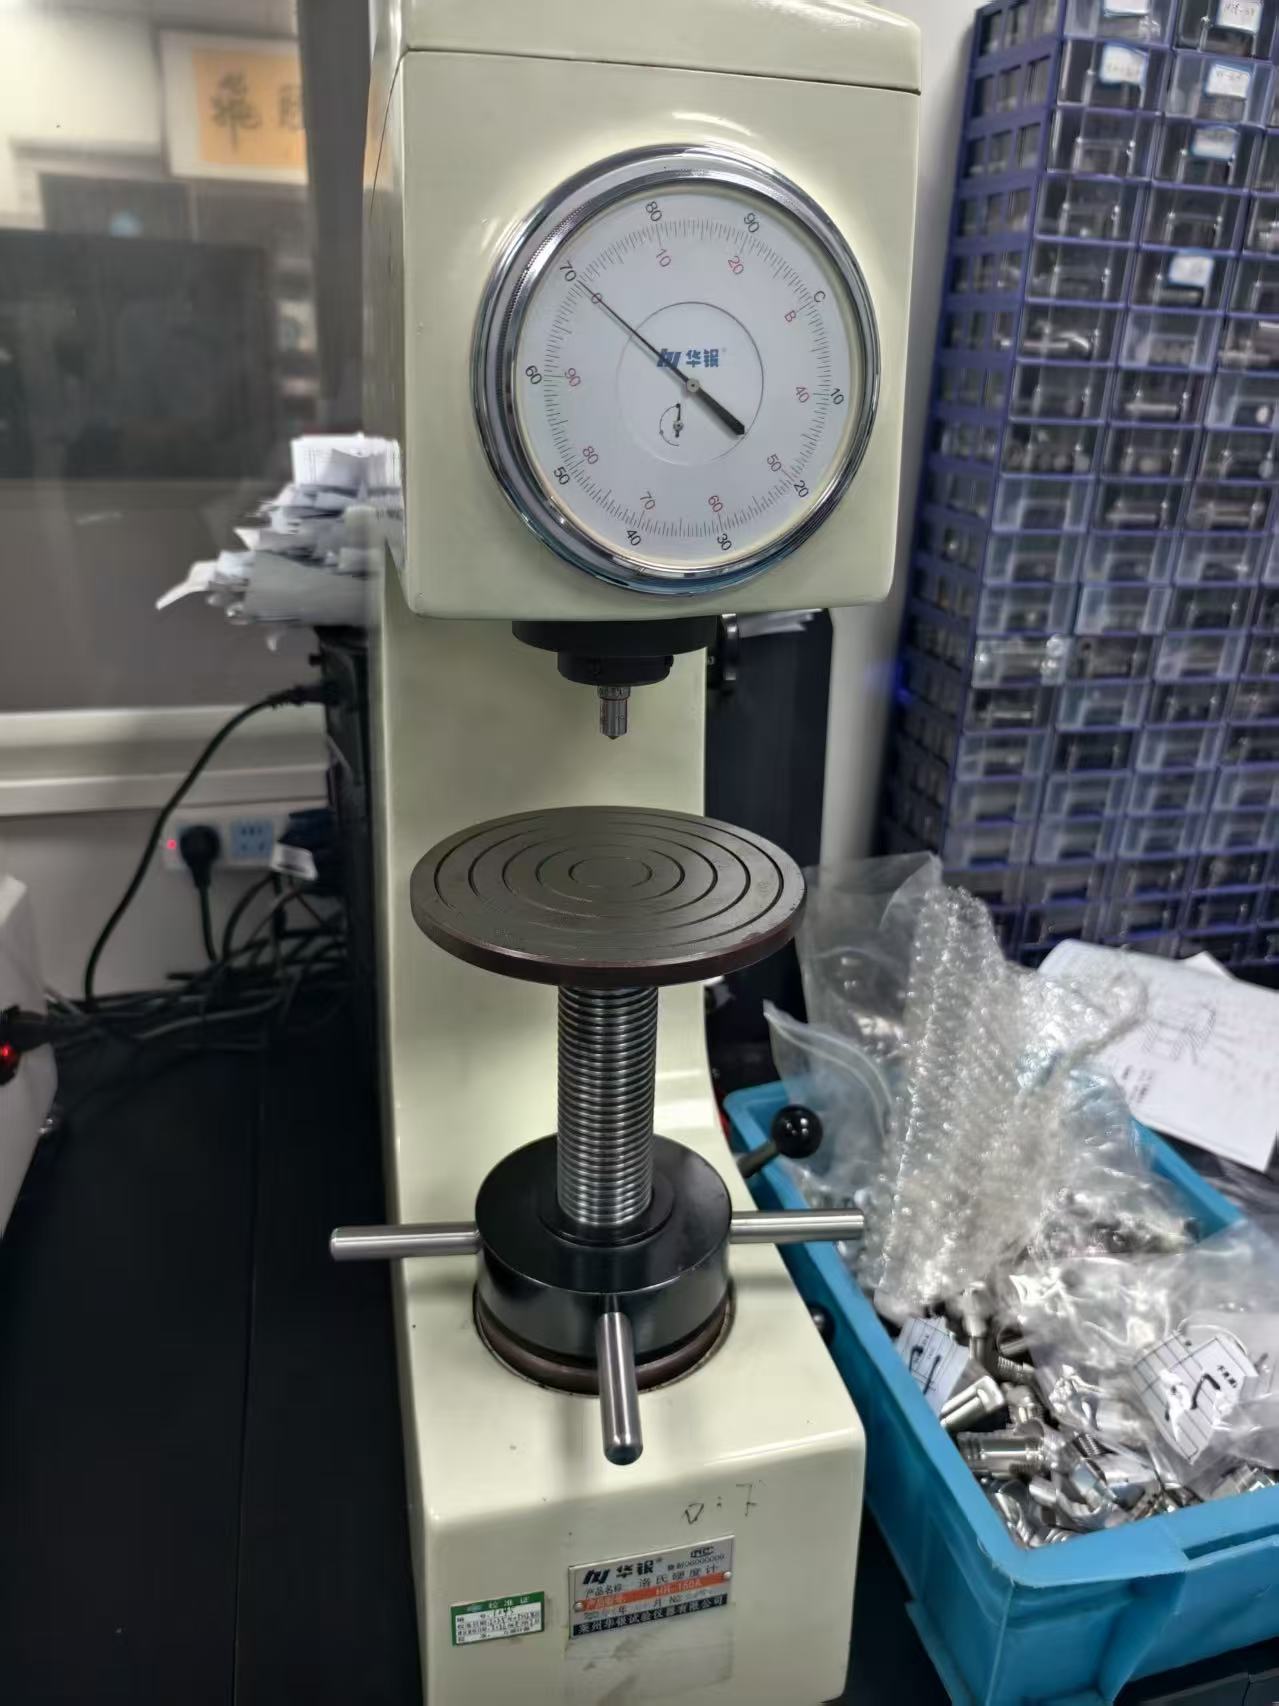
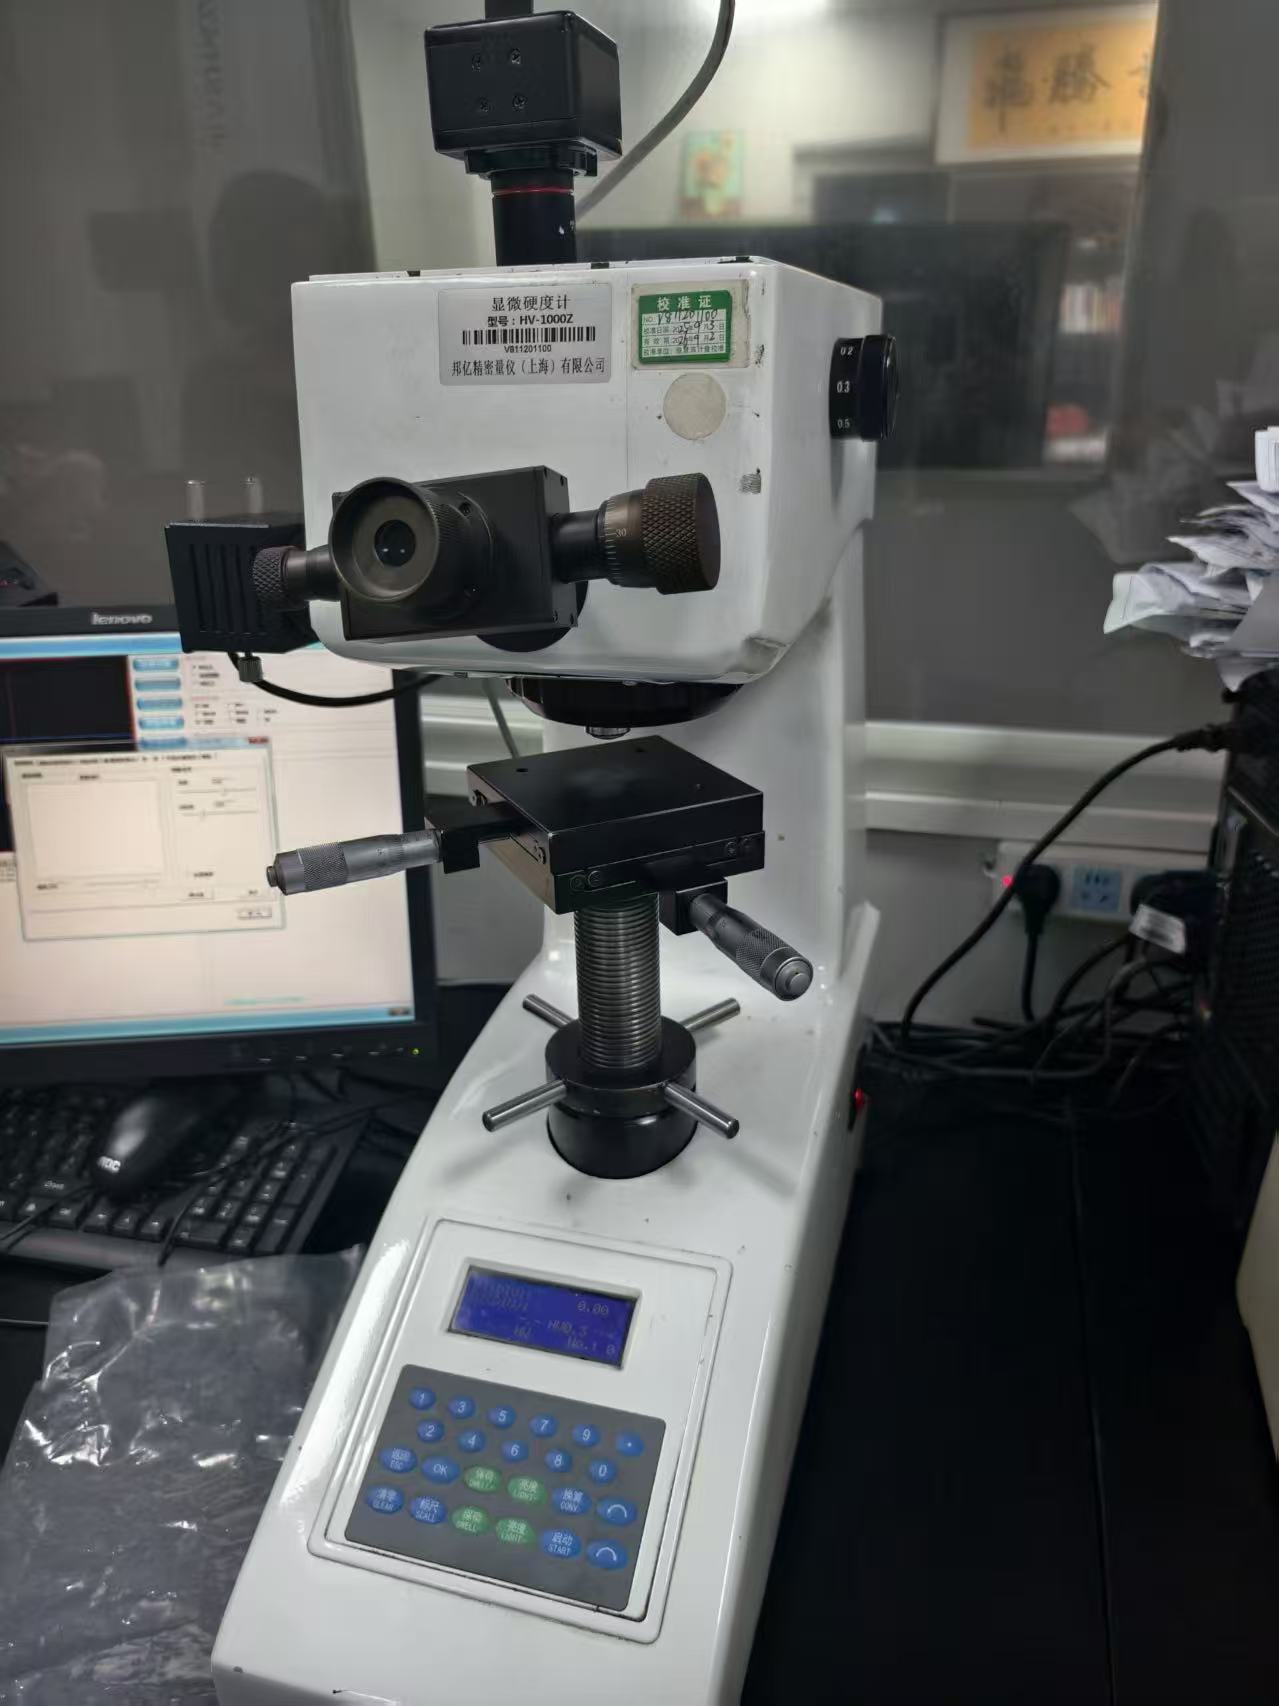
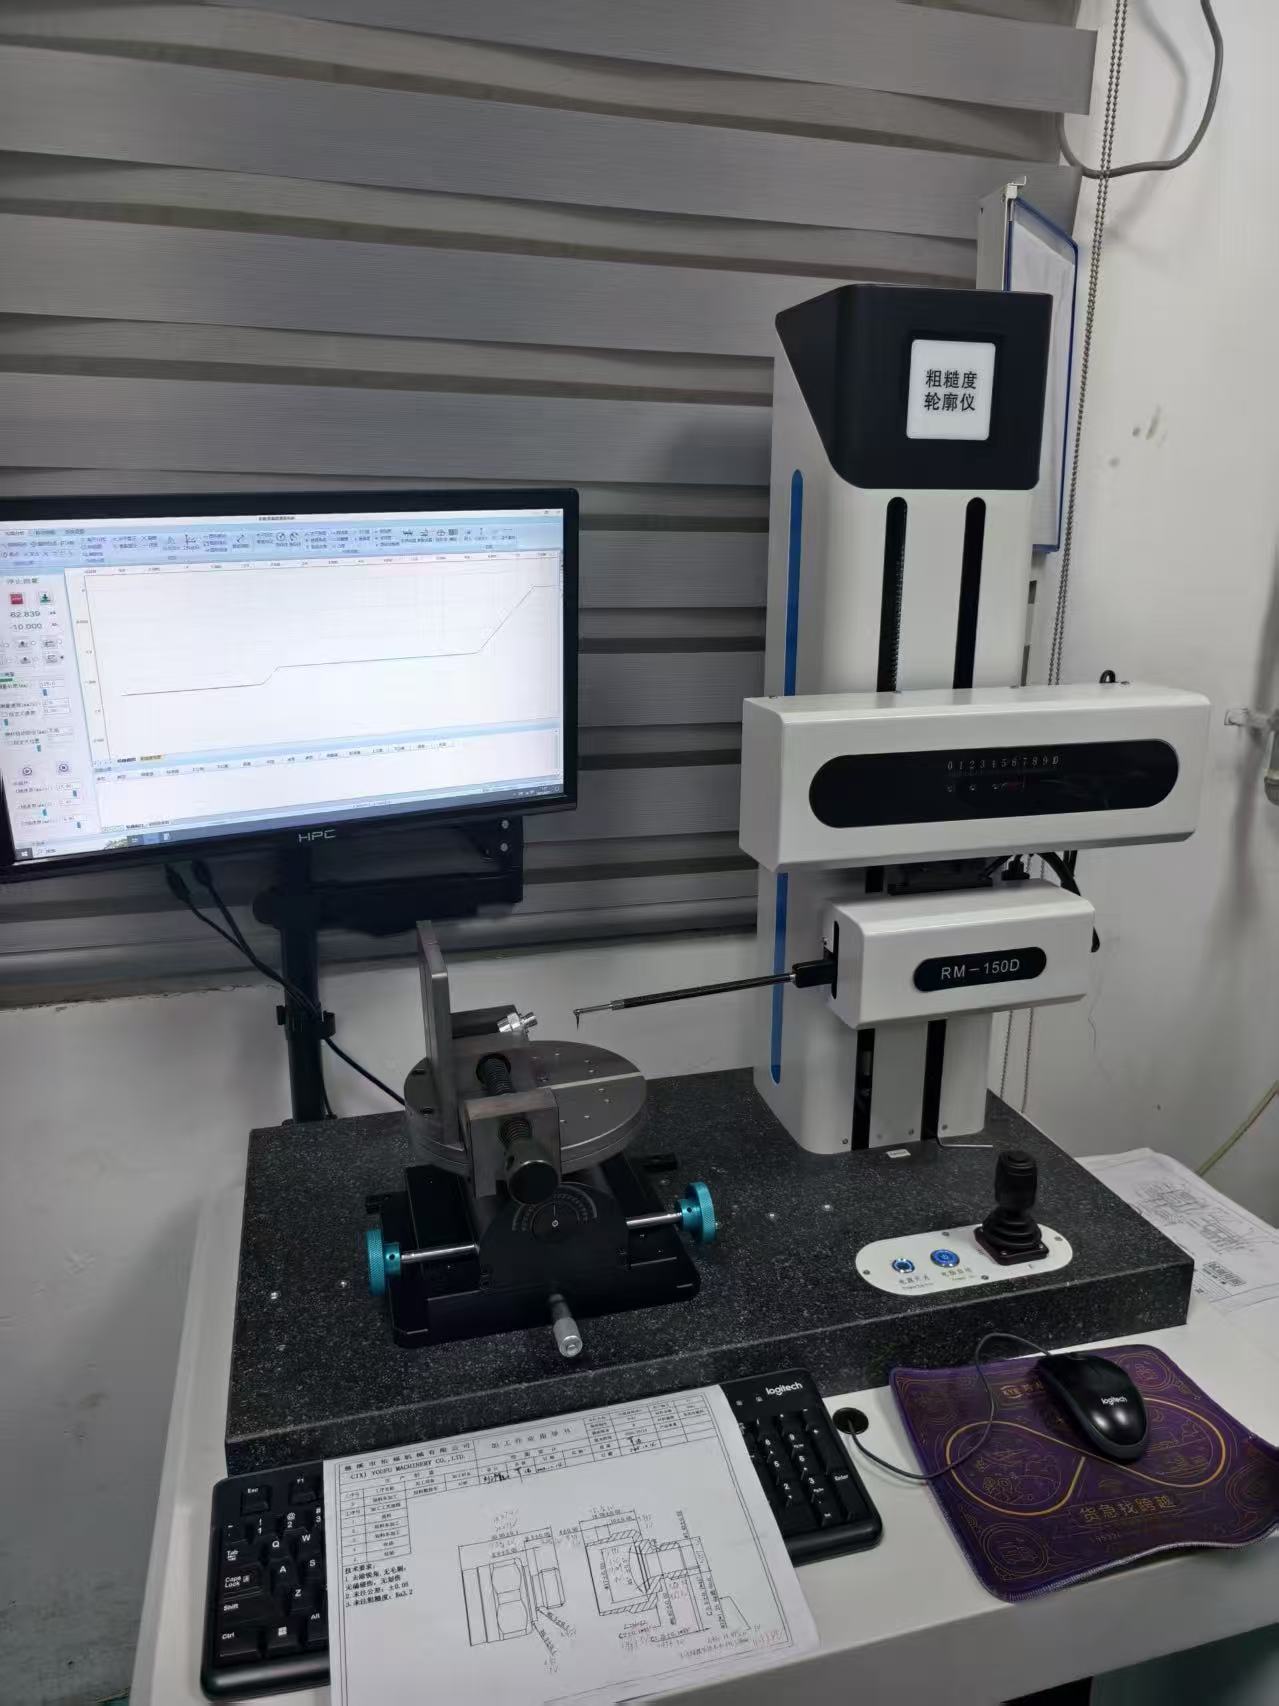
We operate on the principle that quality is engineered in, not inspected in — but we still verify it at every stage. Our inspection lab includes CMM, vision measuring system, contour instrument, surface roughness tester, tensile tester, hardness tester and metallographic microscope.
7. Certifications & Compliance
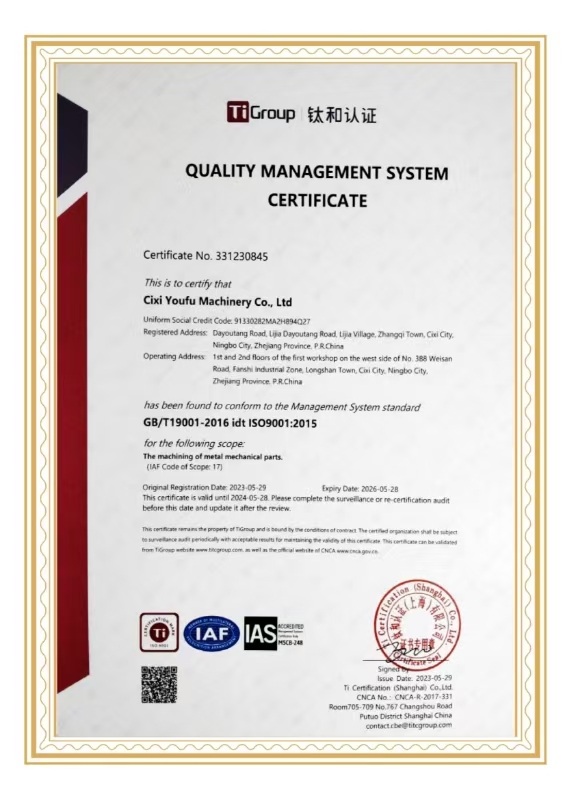
- ISO 9001:2015 (GB/T 19001-2016) — our manufacturing facility is ISO 9001:2015 certified, with scope covering production of metal machined parts.
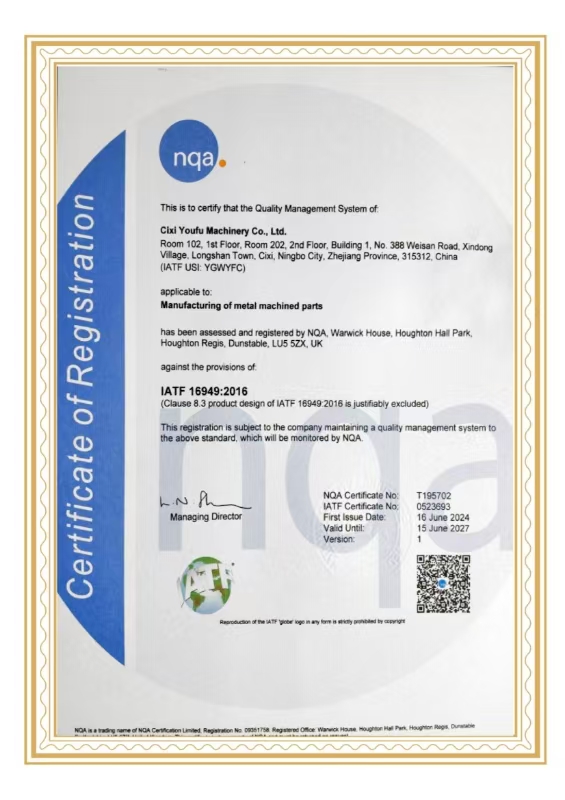
- IATF 16949:2016 — automotive quality management system held by our manufacturing facility, for customers who require automotive-grade process control and full traceability.
- RoHS / REACH compliant materials and finishes.
- Third-party test reports and material certificates available on request.
- 16+ years serving automotive, industrial, agricultural, hydraulic and construction customers in the USA, Korea, Germany, Morocco, Brazil.
8. Real-World Application Scenarios
- Automotive seating systems — stepped positioning dowel pins for seat-slide rails.
- Agricultural and livestock equipment: corrosion-resistant pins and bushings for machines that run outdoors and keep cycling day after day.
- Hydraulic and industrial machinery: hardened, ground pins running in bronze bushings, a pairing that holds up under continuous load.
- Jigs and fixtures: hardened dowel pins and clevis pins, where a few microns of wear throws the whole fixture out of position.
Problems customers bring us most often:
- Turned dowel pins that keep failing fatigue testing. Machining cuts across the grain; cold forming keeps it running with the part, and that’s usually the fix.
- Machined parts that get too expensive once volumes climb. Shift most of the work to cold heading, keep CNC for the finish, and the price drops a lot.
- Bushings that wear out too fast. Getting the bronze grade and surface finish right for the real load and speed usually solves it.
9. Frequently Asked Questions
Q: What is the minimum order quantity (MOQ)?
A: Cold heading rewards volume, but we also run CNC-only for prototypes and low-volume work — from sampling to mass production.
Q: Can you make parts from my drawing or sample?
A: Yes — OEM & ODM from drawing or sample to delivery, including DFM feedback.
Q: What tolerances can you hold?
A: Ground dowel pins routinely hold m6/h6; surfaces reach Ra 0.4–0.8 μm. Send your drawing for confirmation.
Q: Do you provide samples?
A: Yes — samples and first-article inspection (FAI) reports before mass production.
Q: How do you keep batches consistent from one order to the next?
A: We inspect at every stage, not just at the end. Each step gets an in-process check, and the finished batch goes through CMM, vision measurement, hardness testing and the rest of the lab before it ships.
10. How to Get a Quote
- Send your drawing, sample or rough sketch with quantities.
- We reply with DFM feedback, quotation and lead time.
- Approve a sample (with FAI report), then we move to production.
→ Contact us · All products · Custom manufacturing
Conclusion
The days of choosing between “strong,” “precise” and “affordable” are over. Multi-station cold heading combined with CNC finishing delivers components that are stronger at the grain level, tighter in tolerance and cheaper at volume. When you’re ready to put that technology to work on your shaft pins, dowel pins, bushings or fasteners, our 16+ years of in-house cold-forming and CNC experience are at your service.
Shafts that transmit. Fasteners that hold. Bushings that endure.