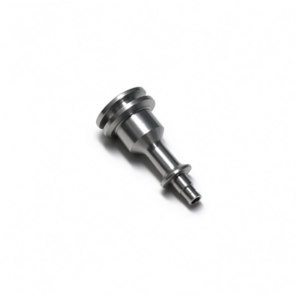
Product Content:
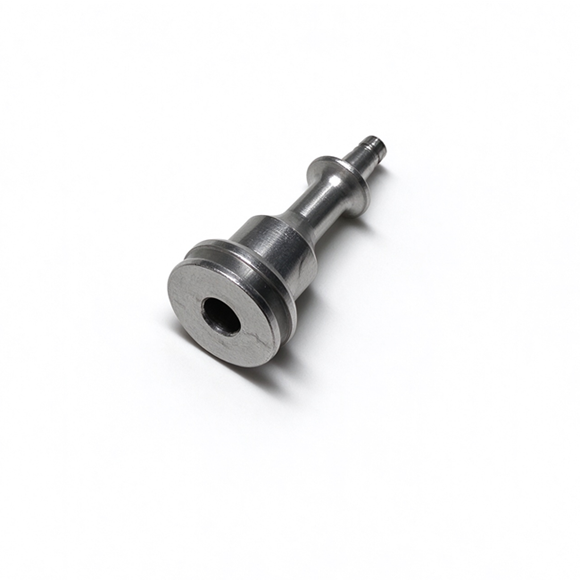
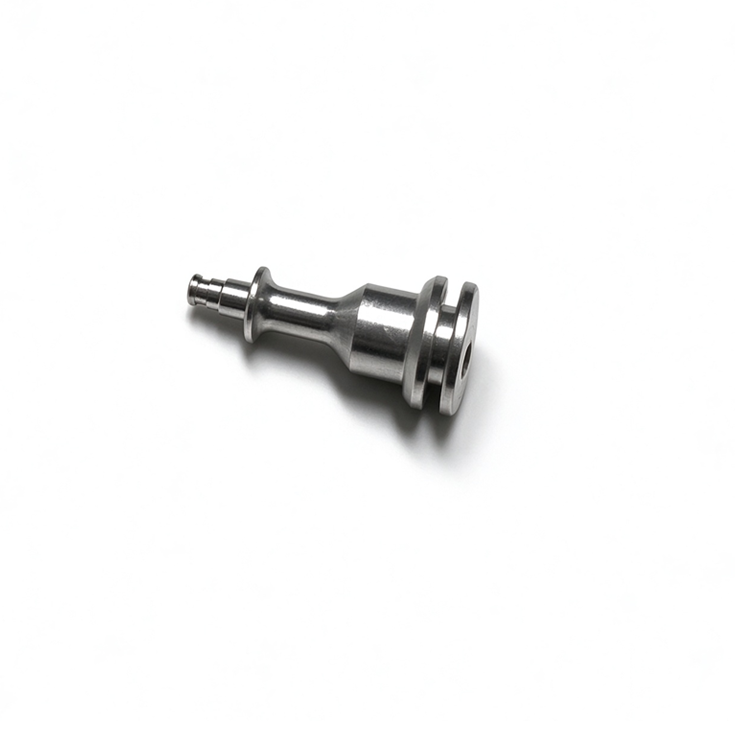
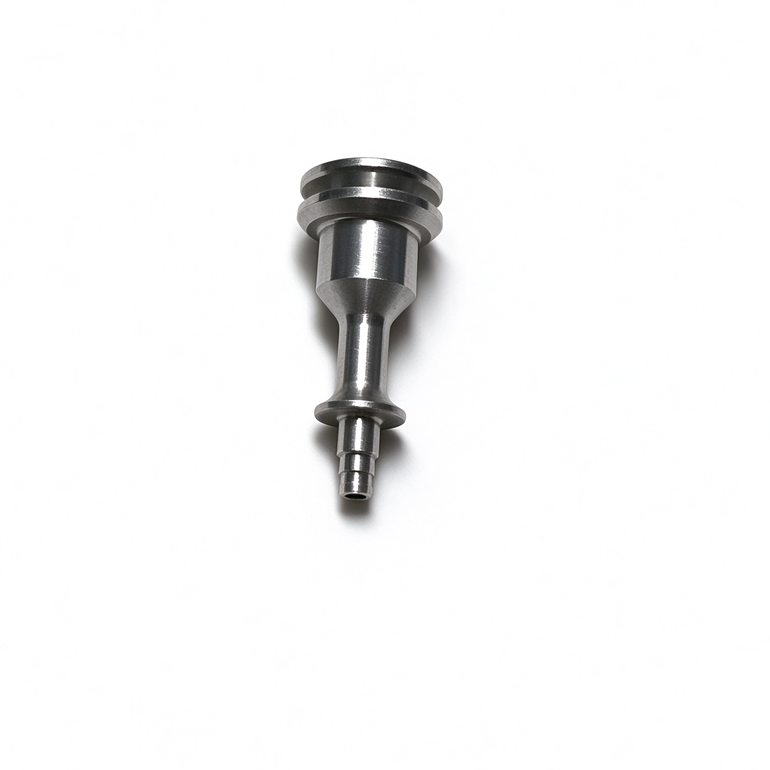
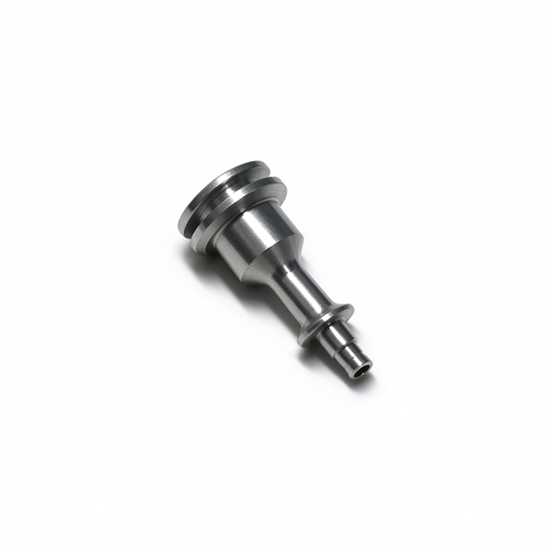
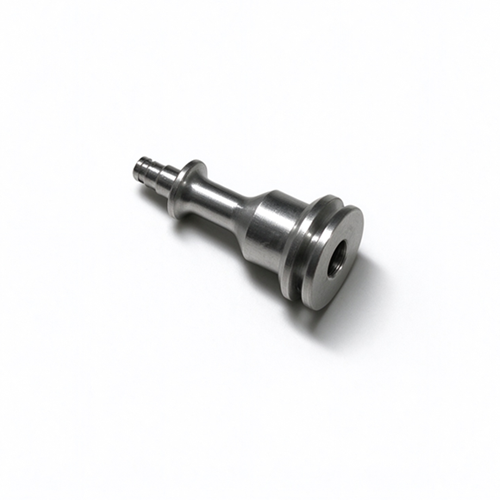
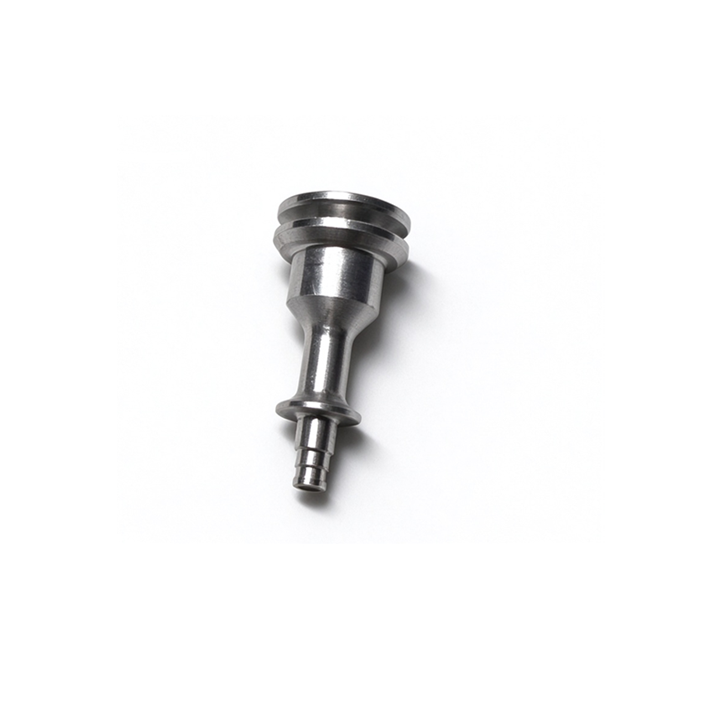
Qimao Metal Manufacturer Valve Pin Manufacturer Precision Ground Valve Pins, Custom is only as good as its shut-off. Ours are ground from H13 or M2 tool steel, then hardened and finish-ground so the tip seats into the gate without leaving flash or a heavy vestige. Shaft straightness is checked before shipment because a pin that runs out will score the bushing and drift off center under heat. We work from your drawing on tip angle, head style and overall length. If you are replacing a worn pin, send the original or a sketch and we will match it.
Product Specification:
| Product Name: | Item No.: | Material: | Measurement(mm): | Surface Finish: | Weight(g): | ||
| L: | W: | D: | |||||
|
Valve Pin Manufacturer Precision Ground Valve Pins, Custom |
QM3002 | Aluminum | / | 6.08/4.14/2.01/3.54/
1.63/:1.39/1.37/1.39 |
Polish | 10.07
|
|
Product Details:
Valve Pin Manufacturer Precision Ground Valve Pins, Custom are ground from H13, M2 or 420 stainless depending on your resin and temperature. Shaft diameter is held to h6 or to drawing, with tip concentricity within 0.01 mm, and straightness is checked on V-blocks to a maximum 0.005 mm runout over the full length. Shaft and tip get a ground finish around Ra 0.4; nitriding is available where abrasion is a concern. Tip geometry — flat, conical or a custom profile — is matched to your gate angle rather than picked from a standard list, and heads can be slotted, threaded or made to drawing. Lengths typically run 50–300 mm, all made to order.
Main Feature:
-
Ground tip seats into the gate cleanly — the Valve Pin Manufacturer Precision Ground Valve Pins, Custom shut-off edge is finished in-house, so flash and vestige stay minimal run after run
-
Straight shaft runs true in the bushing — checked to 0.005 mm runout, which cuts bushing wear and keeps the pin from sticking under heat
-
Hardened H13 or M2 holds the shut-off edge through high cycle counts — the tip keeps its shape instead of rounding off early
-
Custom tip angle matched to your gate geometry — conical, flat or profile ground to your drawing, not a one-size standard
-
Head configurations to suit your actuator or pin holder — slotted, threaded or made to drawing
-
Nitriding available where abrasion is a concern — adds surface hardness without affecting the ground finish
Application:
-
Hot runner systems — the Valve Pin Manufacturer Precision Ground Valve Pins, Custom controls melt flow right at the gate, and shut-off quality decides whether you get a clean gate mark or flash. A worn tip shows up here first, as stringing or drool.
-
Injection molds with valve gating — clean shut-off on engineering resins, including glass-filled grades that chew up soft pins. Hardened H13 or M2 keeps the shut-off edge from rounding off.
-
Replacement pins for worn or damaged originals — send the old pin or a sketch, and we match the tip profile, length and head style. No need to re-engineer the tool around a standard pin.
-
Multi-cavity tools — pin-to-pin consistency matters here. Every pin in the batch is ground to the same tolerance, so one cavity doesn’t gate differently from the next.
-
High-temperature engineering materials — where standard pins soften and lose the edge, H13 or M2 holds up. Tip geometry stays stable through the heat cycle.
Factory Advantage:
Slide the Valve Pin Manufacturer Precision Ground Valve Pins, Custom into the piston or pin holder and secure the locking screw or retainer — hand tight is usually enough. Do not over-torque the holder; it can distort the pin head and throw the tip off center. Before running production, heat the system to processing temperature and check that the tip seats fully into the gate. A cold-set pin will grow when hot, so if you set it tight cold it may bottom out and damage the gate. For existing systems, adjust the pin hot and then back off slightly to leave room for thermal growth. At scheduled maintenance, pull the pin and inspect the tip for wear, galling or a rounded shut-off edge, and check the shaft for scoring.
Reviews
There are no reviews yet.