Product Content:
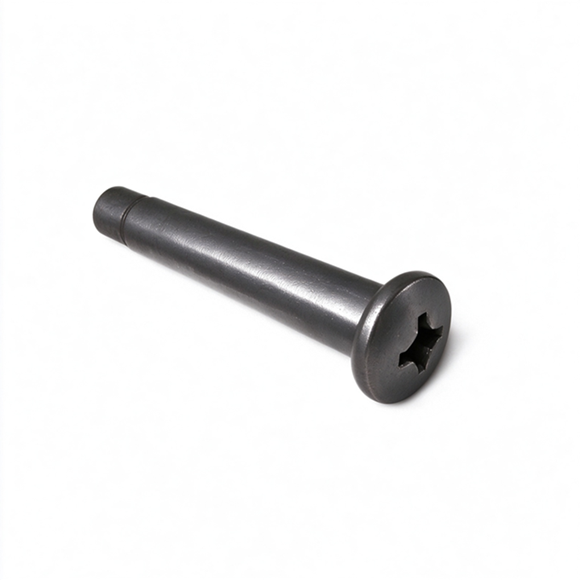
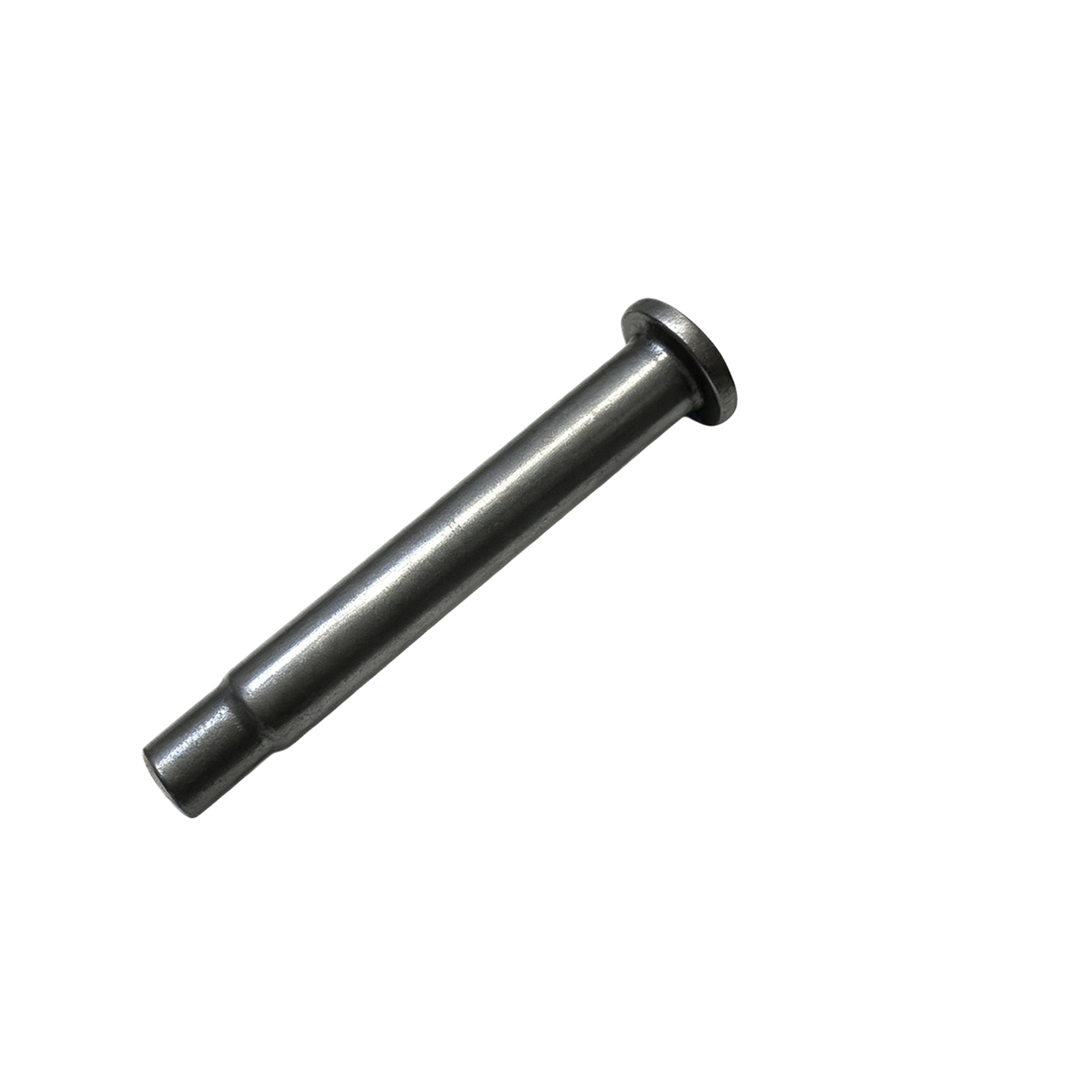
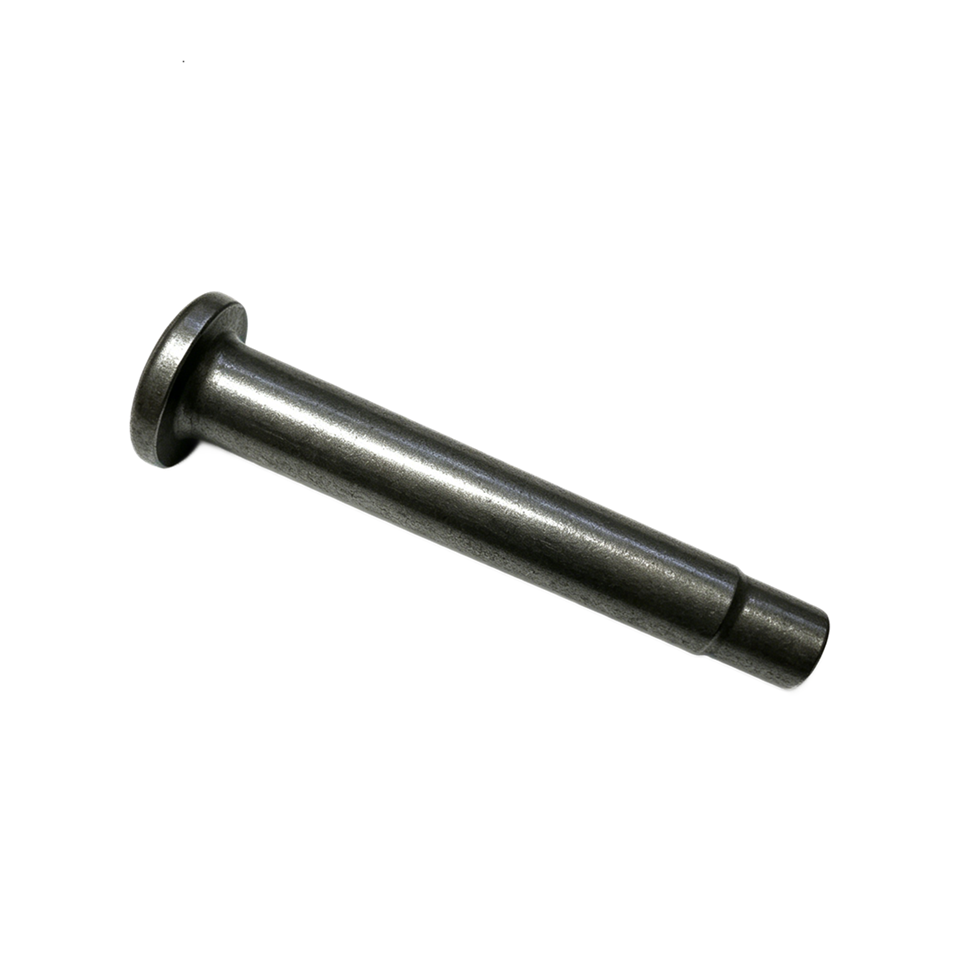
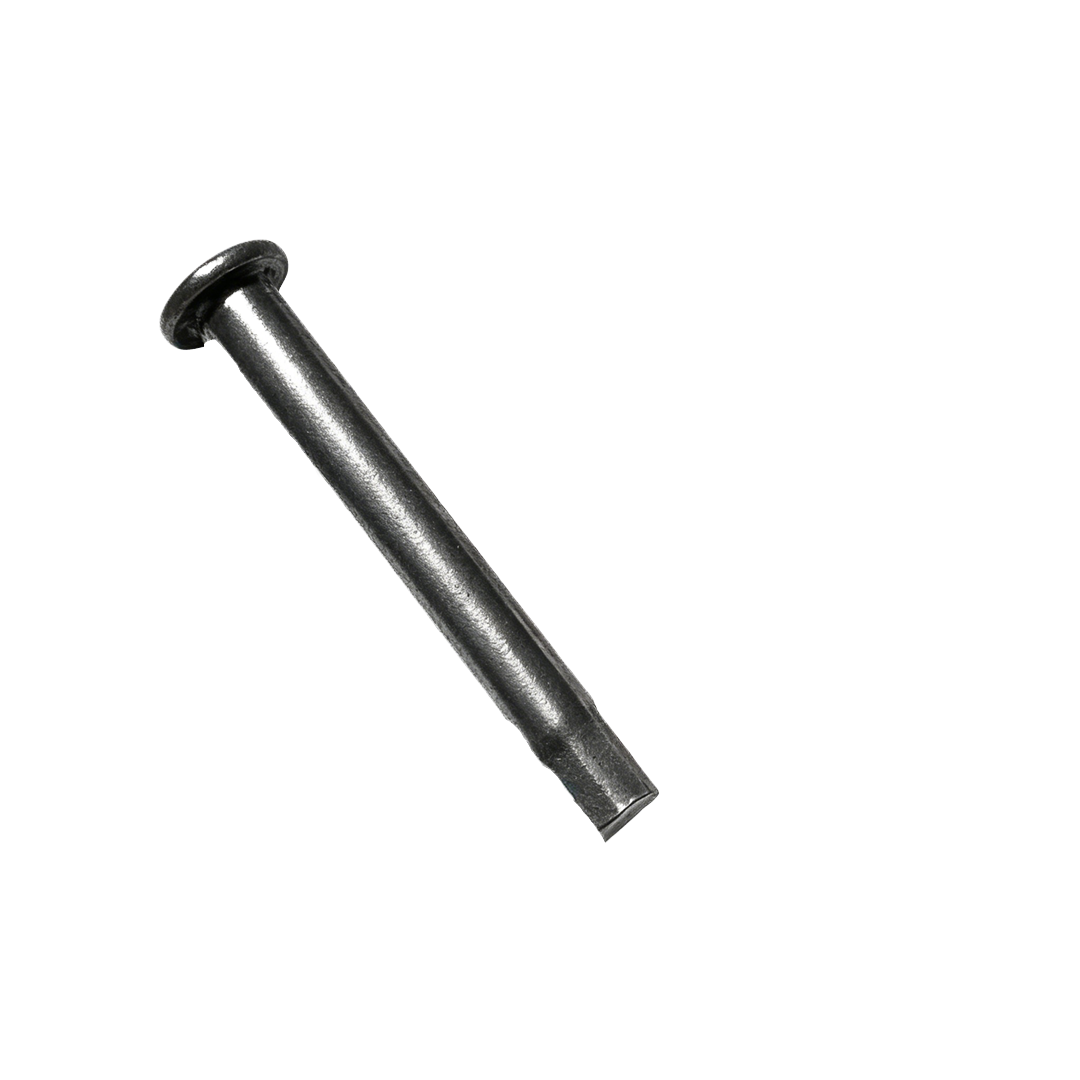
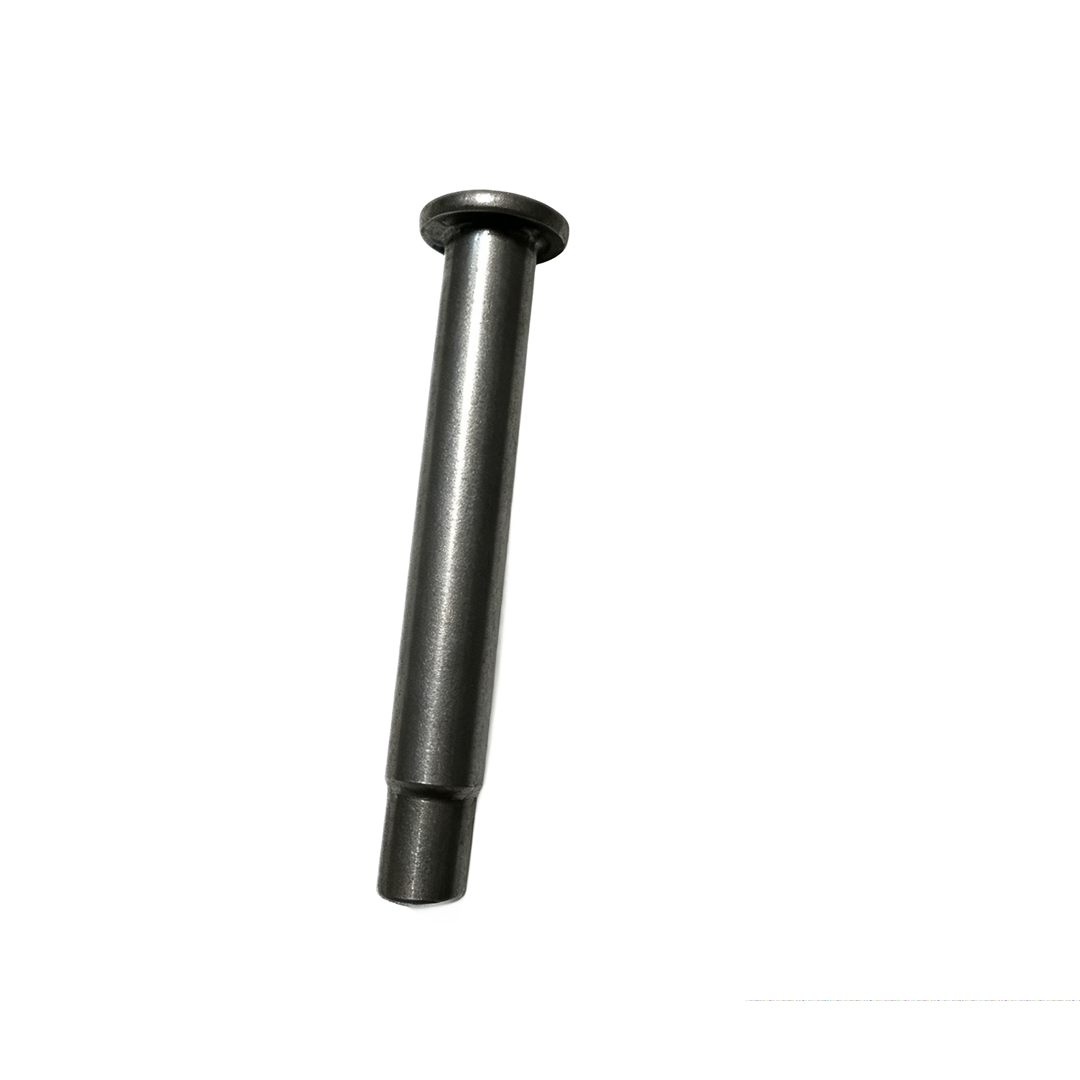
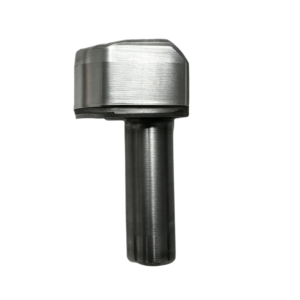
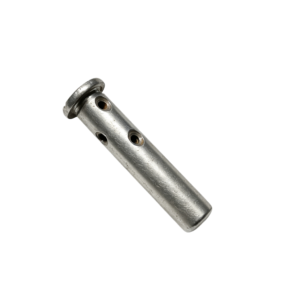
Qimao Metal Manufacturer Custom Cold Heading Flanged Pin Manufacturer – Pumps & Assemblies is cold headed, not machined from bar stock. Wire is cut to length and formed under high pressure into the flanged shape. The metal flows into the die, so the grain structure follows the part contour instead of being cut through. That gives the flange better fatigue resistance than a machined pin, and it keeps material waste low. The flange acts as a stop, locating the pin axially in the assembly. The shank is formed to fit the bore, with diameter and length held to your tolerance. Secondary CNC operations like drilling, threading, or grinding can be added if the part needs them.

Product Specification:
| Product Name: | Item No.: | Material: | Measurement(mm): | Surface Finish: | Weight(g): | ||
| L: | W: | D: | |||||
|
Custom Cold Heading Flanged Pin Manufacturer – Pumps & Assemblies |
QM9051 | Steel | 56.54 | / | 7.8/7.1 | Polish | 21.52 |
Product Details:
For the product Custom Cold Heading Flanged Pin Manufacturer – Pumps & Assemblies made to your drawing or sample. Cold heading is the primary process; secondary CNC machining is available for cross holes, threads, grooves, or ground diameters. Materials include stainless steel, alloy steel, carbon steel, and brass. Key items we control are flange diameter and thickness, shank diameter, overall length, concentricity between flange and shank, and surface condition. Before production, we review the drawing and flag anything hard to form or likely to crack during heading. Prototyping, trial production, and mass production are all supported. Every project gets first article, in-process, and final inspection. Any change in material, process, or supplier goes through ECN and re-verification.
Core Feature:
-
Custom Cold Heading Flanged Pin Manufacturer – Pumps & Assemblies by cold headed from wire, not machined from bar stock. The flange is formed under high pressure in a die, so the metal flows into shape instead of being cut away. Material waste stays low, and production runs fast.
-
Grain flow follows the part contour. Because the metal deforms rather than gets cut, the grain structure runs along the flange and shank. This gives better fatigue resistance than a machined pin, especially at the flange fillet.
-
Flange formed to your diameter and thickness. The flange acts as an axial stop, locating the pin in the assembly. Both flange diameter and thickness are held to your drawing tolerance.
-
Shank formed to fit the bore. Shank diameter and overall length are controlled for proper fit, whether the pin is used for location, pivot, or load bearing.
-
Secondary CNC operations available. If the part needs cross holes, threads, grooves, or a ground diameter, we can add those after cold heading.
-
Material options matched to the job. Stainless steel for corrosion resistance, alloy steel for strength and wear, carbon steel for cost-sensitive high-volume parts, brass for machinability.
Wide Usage:
-
Custom Cold Heading Flanged Pin Manufacturer – Pumps & Assemblies for pumps and pump assemblies
-
Automation equipment and actuators
-
Assemblies that need axial location with a formed flange
-
High-volume parts where cold heading lowers cost per piece
-
Replacement of machined pins in fatigue-sensitive applications
-
Parts that need a formed flange plus secondary machining
-
Small appliance and power tool assemblies
-
Non-standard cases where a standard pin cannot meet assembly requirements
Installation Guide:
When install the item Custom Cold Heading Flanged Pin Manufacturer – Pumps & Assemblies ,first check the pin against the drawing first — flange diameter and thickness, shank diameter, and overall length. Clean the bore and the mating surface before assembly. Insert the pin by hand; it should slide into the bore with light pressure. If it binds, stop and check the tolerance. Seat the flange against its mating surface. After assembly, check that the pin sits square and the flange makes full contact.


Reviews
There are no reviews yet.