Product Description:
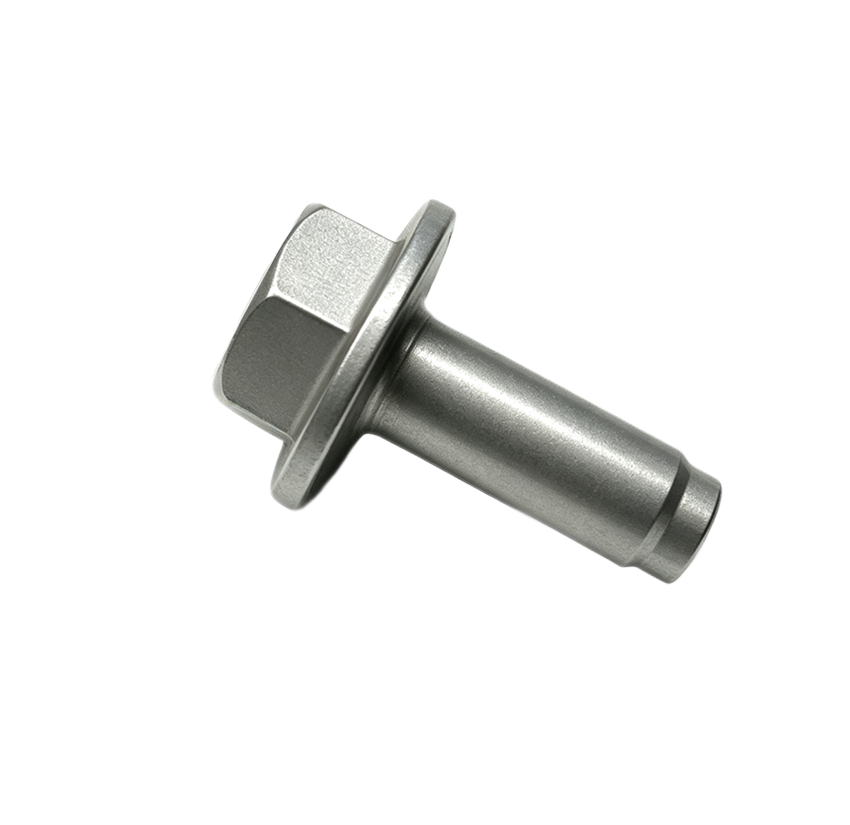
Take a cross-section of Qimao Metal Manufacturer Shoulder Location Pin Manufacturer against one machined from bar. The difference shows at the shoulder fillet. In the headed part, grain lines follow the contour—they bend without breaking. That continuity translates directly to fatigue resistance. The machined version cutting tool severs those same grain lines at the critical radius, leaving a path for crack propagation.
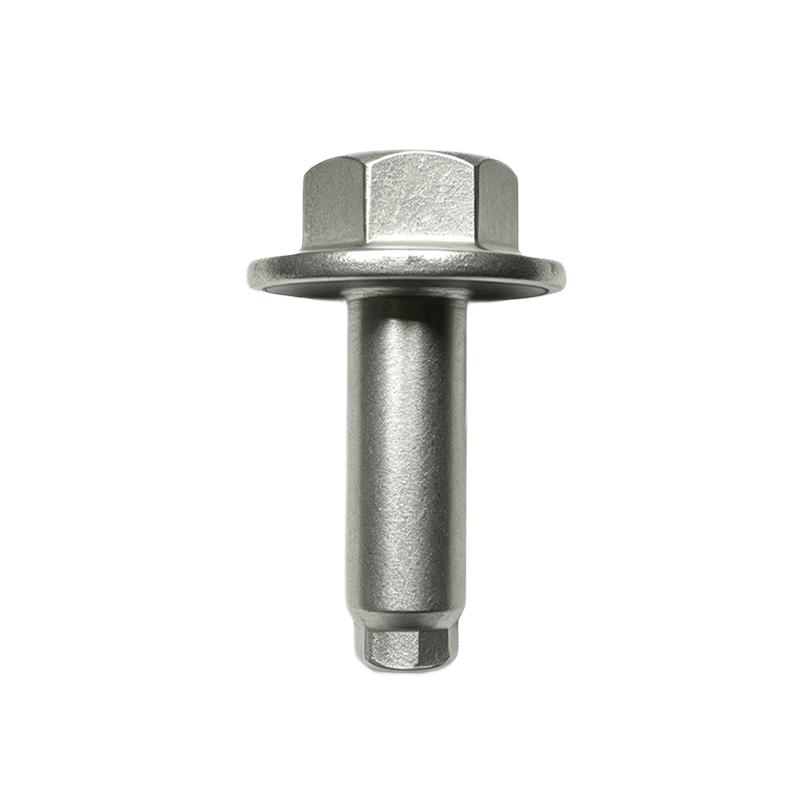
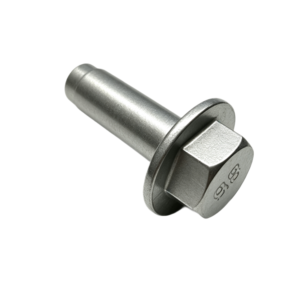
Our heading sequence runs four to six dies depending on complexity. Wire gets sheared to slug length, then upset progressively into the final shape. After that, we do only what’s necessary: grind the locating diameter to ±0.0005, turn the flange face square, and break the entry chamfer. The hex forms in the header—no broaching, no milling. That saves time and keeps cost down. Surface finish on the ground shank runs 16 micro-inches Ra. We check concentricity between the ground diameter and the flange face routinely; our standard is 0.002 TIR.
Specification:
| Product Name: | Item No.: | Material: | Measurement(mm): | Surface Finish: | Weight(g): | ||
| L: | Nut: | Dia: | |||||
| Shoulder Location Pin Manufacturer | QM9052 | Steel | 33.95 | M8 | 9.03/7.48 | Polish | 27.09 |
Products Details:
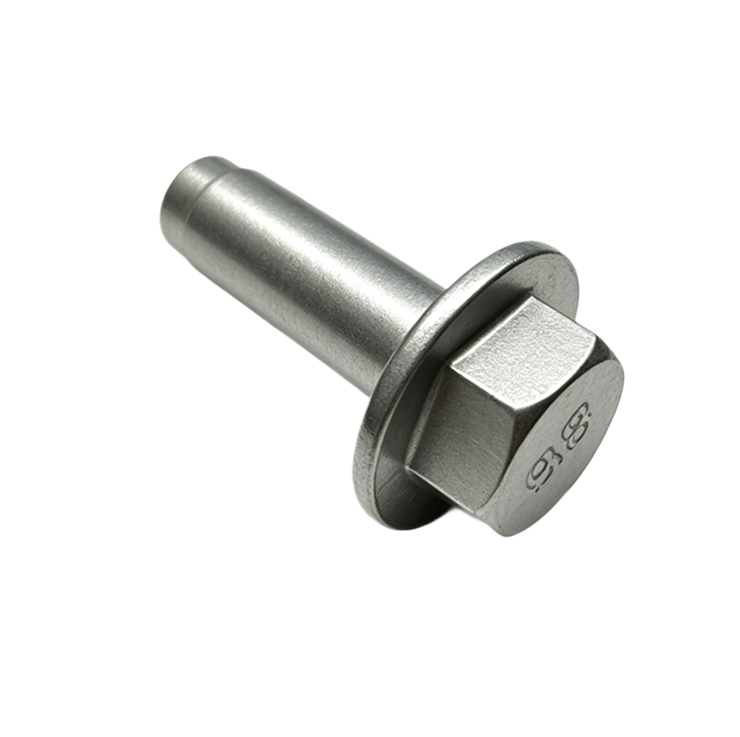
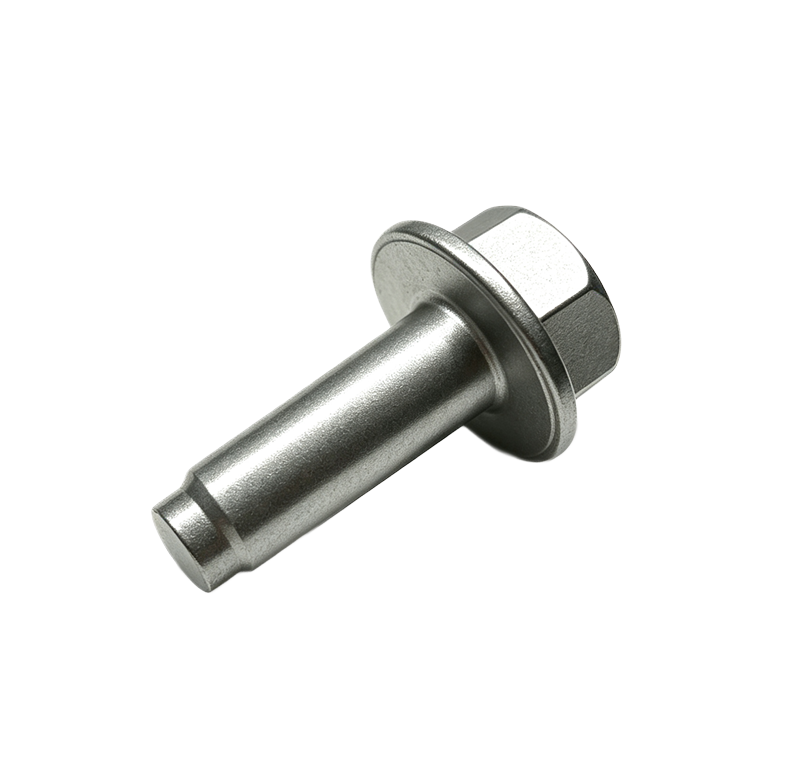
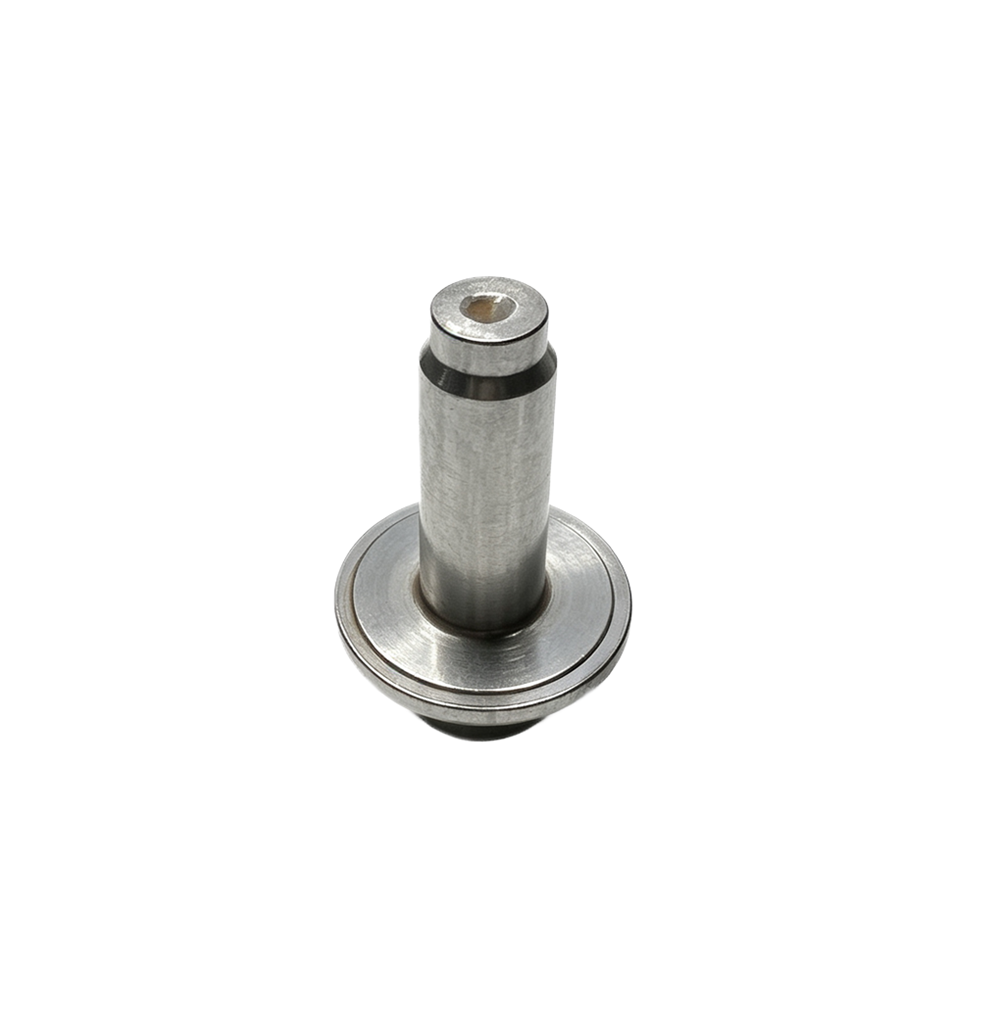
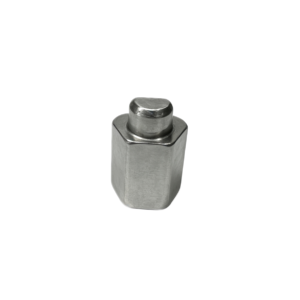
The Shoulder Location Pin Manufacturer thread size is M4, with a 25mm overall thread length. The locating shank features two distinct diameters—9.03mm at the pilot section for precise location, stepping down to 7.48mm at the reduced portion. The 9.03 diameter is the critical locating feature; we hold it to +0.000/-0.005mm, with concentricity between the shank and the flange back face held to 0.02mm TIR maximum—0.01mm achievable on request. Lead-in chamfer is 15 degrees to guide smooth bushing entry. Standard surface finish is black oxide for corrosion resistance, though zinc plating and plain oil finish are available as alternatives. Identification marking on the flange face carries material grade and batch code for full traceability.
Product Feature:
-
Shoulder Location Pin Manufacturer construction. Grain flow follows shoulder contour, not severed by machining. Gives fatigue resistance you don’t get with bar-fed parts.
-
M4 threaded shank, 25mm length. Stepped design—9.03mm pilot, 7.48mm reduced section. Locating precision at bushing, clearance elsewhere.
-
Hex flange formed in header, not broached. Flange face square to shank—concentricity within 0.02mm TIR.
-
Black oxide standard. Zinc plating and oil finish available. Laser mark on flange carries material grade and batch code.
-
15-degree lead-in chamfer. Guides smooth bushing entry without scoring bore or damaging pilot.
Product Application:
-
Shoulder Location Pin Manufacturer used for automotive welding fixtures. Locates stamped panels before robotic welding. High cycle counts—cold heading handles the wear.
-
Machining center pallet systems. 9.03mm pilot engages bushing, 7.48mm portion provides clearance for chip evacuation.
-
Inspection fixtures and hard gauging. Ground diameter and square flange give reliable datum for casting verification.
-
Jig repairs and changeouts. M4 thread and hex flange mean straightforward replacement. No special extractors needed.
-
Flexible tooling setups. Standard hex dimensions mean same wrench fits multiple sizes. Custom heights ship within 3-4 weeks.
Reviews
There are no reviews yet.